


Производител на работни станции за роботи и лазерни системи по поръчка



Продавам позиционер за заваряване: Как да изберете правилния тип за вашата част (Главна стойка Задна стойка, L-тип, U-тип, Хоризонтална 3-осна, Въртяща се с една ос, Вертикално накланяне)
Въведете „позиционер за заваряване за продажба“ и ще получите стотици обяви – Позиционер за задна стойка, L-тип заваръчен позиционер, U-образен позиционер за заваряване, Хоризонтален 3-осов ротационен позиционер, Ротационен позиционер с една ос, and Vertical Tilting Positioner—most described by payload and price alone. Payload is the wrong first filter. The right first filter is your part: its shape, its weight distribution, and the joints you actually need to present in the flat (1G/1F) позиция. This article is a buyer’s guide to choosing the right welding positioner type for your workpiece, drawn from ROBOPTIX field deployments across structural steel, съд под налягане, and heavy-equipment fabrication. We cover the six positioner families ROBOPTIX builds, the load and accuracy checks that matter, and a selection checklist you can drop straight into your next RFQ.
A welding positioner for sale is only a good buy if it can physically rotate your specific part into the position where welding is easiest. That sounds obvious; it is the step most procurement tables skip. The machine type—not the brochure—decides whether your joint ends up flat or fighting gravity, and whether your operator is welding downhill or wrestling the pool uphill . Start with geometry; end with the spec sheet.
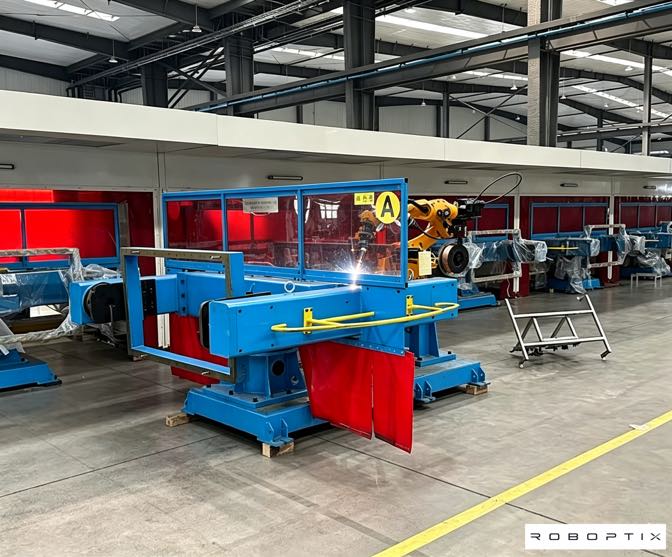
Why Type Selection Beats a Payload Filter
The job of any welding positioner is to move the joint into the flat position so gravity stabilizes the molten pool instead of fighting it. Whether that is even possible depends on the machine’s motion axes, not its payload number. А 2,000 kg rating tells you the axis can rotate a centered mass; it says nothing about a 1,500 kg част, чийто център на тежестта се намира 0.8 m off the rotation axis—where the real overturning moment is what binds the selection. Filter by part first, by payload last.
Concrete example: two suppliers quote you a “2,000 kg welding positioner for sale.” Supplier A offers a Headstock Tailstock Positioner; Supplier B offers an L-Type Welding Positioner. If your part is a 3 m I-beam that needs all four faces welded, Supplier A’s unit cannot present three of those faces at all—payload is irrelevant because the rotation axis that would reach them does not exist. The type, not the number, decides the outcome. That is why this guide leads with geometry and ends with the spec sheet, never the reverse.
Второ, the type decides coordination. If the positioner must move as an external axis with your robot, you need a servo positioner with a controller that declares external axes cleanly—available across the ROBOPTIX B008–B012 multi-axis range. A cheap single-axis gearbox may hold your part, but it cannot coordinate, and that limitation shows up the day you try to weld a seam that needs both machines moving at once.
The Six ROBOPTIX Positioner Families
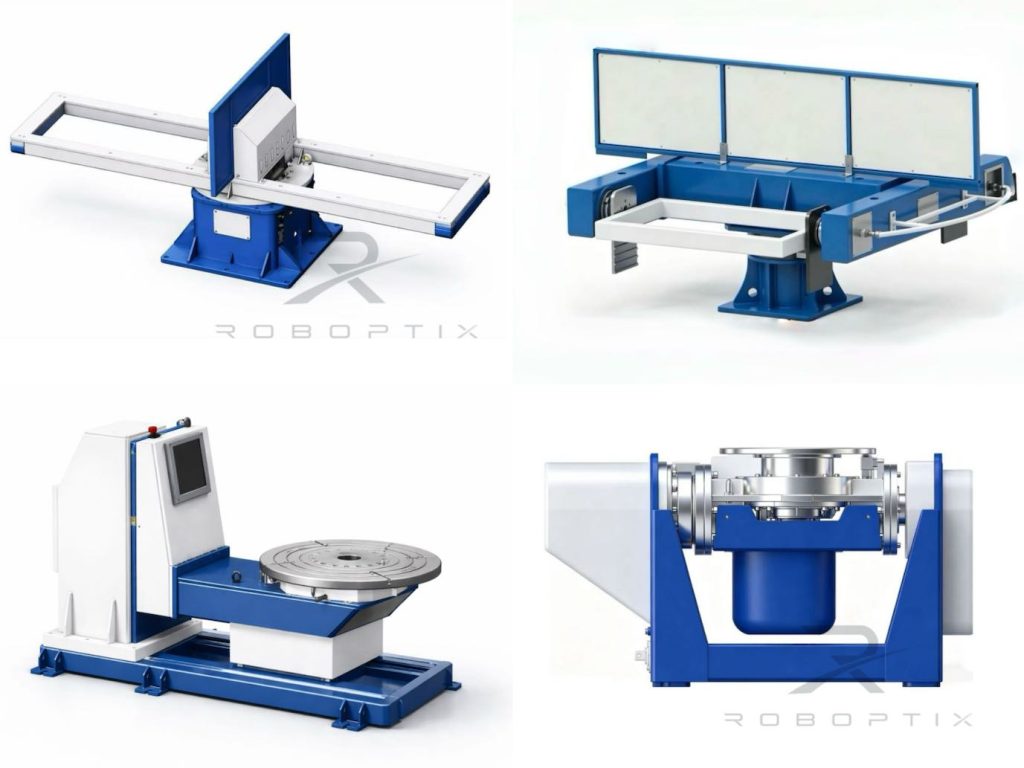
ROBOPTIX builds six positioner families, none of them turning rolls (we rotate the part between driven centers, on a rotary table, or on a tilt/flip axis—never on idle rollers). Pick the family from your part’s dominant geometry, then size it on moment and accuracy.
Позиционер на задната част на главата
Two opposing centers rotate a long part about its own axis: a driven headstock and an idler tailstock. Best for shafts, тръби, тръби, черупки на съдове под налягане, and wind-tower sections where the seam runs along the axis and only rotation—not tilt—is needed. The part is cradled between centers and spun; this is how you weld a cylinder without a crane and without turning rolls. Size it on maximum between-centers mass and the cantilever moment at the tailstock, not just total weight.
Ротационен позиционер с една ос
A single rotary axis—a rotary table or faceplate—spins the part about one axis with the part mounted on its face rather than cradled between centers. Best for flanges, rings, discs, circular plates, and round parts that need only rotation (not tilt) and mount on one face. It is the simplest, most affordable family; size it on table load capacity and the radial moment of the mounted part. Choose it over a Headstock Tailstock Positioner when the part is disc- or ring-shaped and mounts on a face, not between centers.
L-тип заваръчен позиционер
An L-shaped configuration combines a horizontal rotate axis with a vertical tilt axis, so a long part can both spin and flip to vertical. Best for beams, кутии, рамки, and plate assemblies that need multiple faces welded in one mount. The L geometry gives clearance for long sections while still presenting any face flat. If your part has four weldable faces and you are tired of re-fixturing, an L-Type Welding Positioner is usually the answer.
U-образен позиционер за заваряване
A U-shaped frame cradles the part on a combined tilt-and-rotate axis with an open envelope. Best for large, bulky, or irregular frames and weldments too big or awkward for an L-Type Welding Positioner. The open U gives clearance for large sections, приспособления, and tooling, and typically carries a higher overturning-moment rating for heavy, off-center loads. Choose U-Type over L-Type when the part’s footprint or mass exceeds what the L-Type can cradle safely.
Хоризонтален 3-осов ротационен позиционер
Tilt plus rotate plus a linear or secondary rotate axis lets the controller orient almost any contour. Best for complex, multi-orientation seams—castings, mixed-geometry weldments, and parts where one flip or rotate cannot reach every joint. The ROBOPTIX B008–B012 multi-axis servo units sit here, with the accuracy to hold a seam through continuous reorientation. This is the family to specify when no simpler type fits.
Вертикален накланящ се позиционер
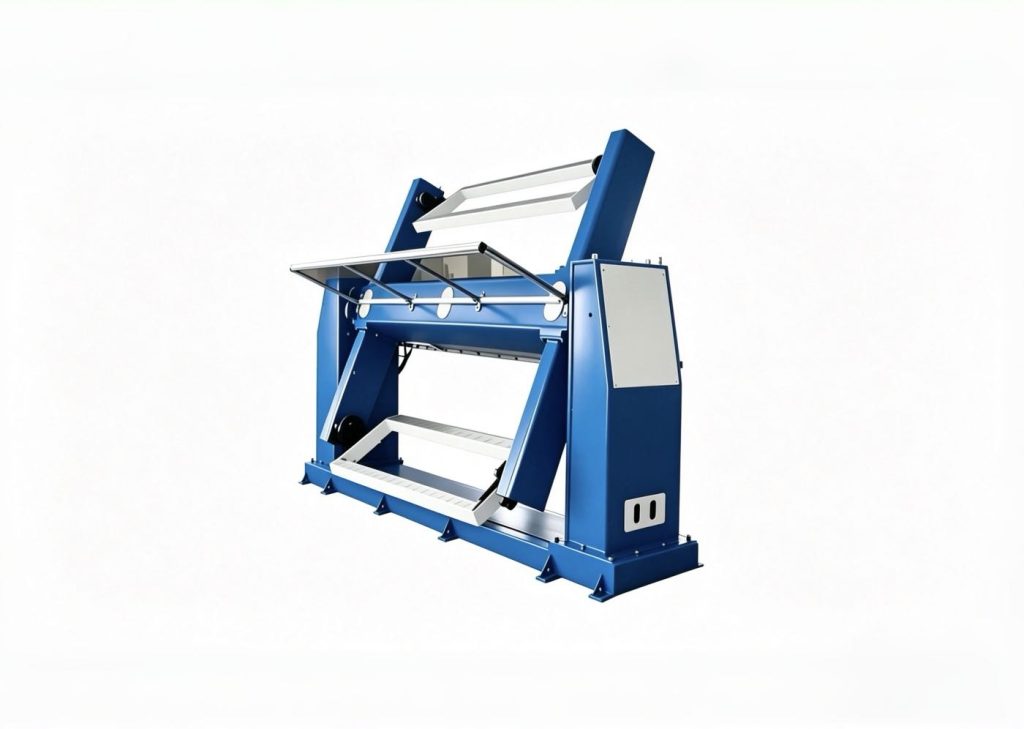
A flip/tilt axis turns the part end-over-end or up-end to present the opposite face, usually combined with a rotate axis. Best for heavy plate and box sections that must be flipped to weld both sides without a crane. The flip removes crane cycles, заваръчни шевове, и handling time , and it keeps the joint flat on the second side instead of forcing an overhead weld . For heavy plate, a Vertical Tilting Positioner is often the single biggest throughput gain available.
The Three Checks That Decide the Type
Geometry First
Map the part to a family before reading a spec sheet.
Long and rotational (between centers) → Headstock Tailstock Positioner.
Round disc or ring (mounted on a face) → Single Axis Rotary Positioner.
Long and multi-face → L-Type Welding Positioner.
Large and irregular → U-Type Welding Positioner.
No single simple orientation reaches every seam → Horizontal 3-Axis Rotary Positioner.
Heavy plate needing both sides → Vertical Tilting Positioner.
The comparison table below makes this a one-glance decision.
Load and Overturning Moment
Once the family is chosen, size it on moment, не маса. Compute overturning moment as weight multiplied by the distance of the center of gravity from the rotation axis, and add inertia for the duty speed. A positioner that is perfect on paper for a centered 2-ton part can fail silently on a 1.5-ton part hung off-center. State the moment and the inertia in the RFQ; make the supplier size to those, not to the brochure payload.
Hidden Specs: Луфт, Скованост, Drift
The number that sells the welding positioner is rarely the number that welds it. Backlash at direction reversals, torsional stiffness under side load, and thermal drift over a duty cycle decide real seam quality. Ask the supplier to demonstrate—or let you measure—backlash at a reversal and stiffness under load. If they have no method to show these, това отсъствие само по себе си е отговорът, and it tells you how much of the spec sheet is measurement versus marketing.
Accuracy and How to Verify It
Accuracy is reported, не се предполага. ROBOPTIX is ISO 9001-certified and reports welding positioner accuracy using ISO 9283:1998-aligned metrics—pose accuracy AP and pose repeatability RP—so the numbers mean the same thing across suppliers. For tight tolerances, support third-party or on-site laser-tracker verification per ISO 9283, with your part mounted and at operating temperature, not just an empty cold run. Условията са бройката; a repeatability figure without its load, температура, and speed is a half-truth.
Positioner Type Comparison
For the full spec-by-spec breakdown across all six families, see the dedicated comparison Welding Positioner Types: Side-by-Side .
| семейство | Best workpiece | Брадви | Payload class |
| Главна стойка Задна стойка | Shafts, тръби, vessel shells, long cylinders | Rotate | Light–heavy, дълго |
| Въртяща се с една ос | Фланци, rings, discs, circular plates (rotate only) | Rotate (one axis) | Лек–среден |
| L-тип | греди, кутии, рамки, чинии (многолицев) | Накланяне + завъртане | Лек–среден |
| U-тип | Large, bulky, irregular frames | Накланяне + завъртане | Средно тежък |
| Хоризонтална 3-осна | Отливки, mixed complex seams | Накланяне + завъртане + linear/2nd rotate | Средно тежък |
| Вертикално накланяне | Тежка плоча, box sections (двете страни) | Flip/tilt + завъртане | Средно тежък |
Работени примери
Structural Beam (long I-beam, four faces)
An I-beam needs all four faces welded. A Headstock Tailstock Positioner only spins it, leaving three faces unreachable. An L-Type Welding Positioner tilts the beam to vertical and rotates it, presenting each face flat in one mount—no re-fixturing, no crane. This is the textbook L-Type case.
Обвивка на съд под налягане (long cylinder, axial seam)
A cylindrical shell with a seam along its axis needs only rotation. A Headstock Tailstock Positioner spins it between driven and idler centers—no turning rolls, no crane—keeping the circumferential and longitudinal welds in the flat position . Дълги, uniform, rotational: Headstock Tailstock is the right and cheapest fit.
Flange or Circular Plate (rotate only)
A flange or circular plate needs only rotation about its axis, mounted on a face rather than cradled between centers. A Single Axis Rotary Positioner spins it on a rotary table or faceplate—no tilt, no flip, the simplest and most affordable fit. For a ring or disc, choose Single Axis Rotary over a Headstock Tailstock Positioner; for a long cylinder, choose the reverse.
Irregular Casting (mixed seams, no single orientation)
A casting with seams on faces that no single flip reaches needs continuous reorientation. A Horizontal 3-Axis Rotary Positioner (ROBOPTIX B008–B012) holds the part and orients each joint flat in turn. No simpler family can do it; specifying a 3-axis here prevents the mis-spec penalty of buying a machine that cannot reach the work.
Beyond the Positioner: Build the Cell
The positioner is one axis of a cell, not a standalone machine. ROBOPTIX pairs it with a 7th Axis Robot Rail System that extends robot reach and a Robot Base / Robot Pedestal that gives the whole cell a stable foundation . Built around that platform are complete, application-ready workstations: coordinated welding cells, no-programming vision-guided cells and turnkey workstations for welding, лазер , handling and palletizing , portable collaborative units and remote mobile systems . When your part does not match a catalog shape, our custom positioner program builds it to the geometry . Because ROBOPTIX is ISO 9001-certified and typically priced 50–70% below equivalent overseas-brand units while reporting accuracy per ISO 9283:1998 methodology, the positioner is rarely the budget problem—specifying the wrong type is.
Your RFQ Checklist: Send Us These 6 Inputs
This checklist is the short version for your RFQ. For the complete buyer’s checklist—budget bands, acceptance criteria, and red flags—see Контролен списък за закупуване на позиционер за заваряване.
The introduction promised a checklist you can drop into an RFQ. Here it is. Send these six inputs and ROBOPTIX will return a type-and-moment specification before you buy—no obligation, and no paywall hiding the math (P09). The more complete the input, the tighter the spec; a one-line “send welding positioner for sale quote” email almost always comes back as the wrong machine.
| Вход | What to send | Why it decides the type |
| Part drawing (2D/3D) | СТЪПКА, DWG, or PDF with dimensions and weld-joint locations marked | Reveals dominant geometry → which of the six families fits |
| Mass + център на тежестта | Total weight and CoG offset from the rotation axis | Sets overturning moment, not just payload |
| Duty cycle & скорост | Welds per shift, rotations per minute, accel/decel profile | Drives inertia, скованост, and thermal-drift sizing |
| Лента за толерантност | Required pose accuracy AP / повторяемост RP | Decides servo grade and ISO 9283:1998 verification need |
| Създаване на робот & interface | Марка, controller model, external-axis protocol | Confirms clean coordination as an external axis |
| Целева пропускателна способност | Parts per hour and handling/fixturing time budget | Flags where a Vertical Tilting Positioner or 7th Axis Robot Rail System removes crane cycles |
A complete RFQ also tells us the budget envelope and any non-standard constraints—ROBOPTIX supports non-standard customization and is ISO 9001-certified, typically priced 50–70% below overseas-brand equivalents while reporting accuracy per ISO 9283:1998 methodology. Send the six inputs above and we will tell you the family, the moment rating, and the acceptance criteria in writing.
When a Positioner Isn’t the Answer
A welding positioner for sale is not always the right buy. For small parts an operator can flip by hand, for loose tolerances (±1 мм), or for genuine high-mix, low-volume work, the fixture-free and manual approaches often win on total cost. Audit any new supplier before committing, and weigh the five-year total cost of ownership against the sticker—the cheap quote is often the expensive machine. Spend on the positioner where the part justifies it; пропуснете го там, където не го прави. присъда, не ритуал, защитава бюджета.
Често задавани въпроси
Q: Which type of welding positioner do I need?
А: Start from your part’s geometry, not the payload. Long rotational parts (валове, тръби, vessel shells) want a Headstock Tailstock Positioner; round discs and rings mounted on a face want a Single Axis Rotary Positioner; long multi-face parts (греди, рамки) want an L-Type Welding Positioner; large irregular frames want a U-Type Welding Positioner; mixed complex seams want a Horizontal 3-Axis Rotary Positioner; heavy plate needing both sides wants a Vertical Tilting Positioner. Then size on overturning moment and verify accuracy per ISO 9283:1998.
Q: What is the difference between a Headstock Tailstock Positioner and an L-Type Welding Positioner?
А: A Headstock Tailstock Positioner rotates a long part about its own axis only—ideal for cylindrical seams. An L-Type Welding Positioner adds a tilt axis, so the part can also flip to vertical and present multiple faces flat in one mount. If your part has more than one weldable face, the L-Type removes re-fixturing that a Headstock Tailstock Positioner cannot.
Q: When do I choose a Single Axis Rotary Positioner instead of a Headstock Tailstock Positioner?
А: Both rotate the part about one axis, but a Single Axis Rotary Positioner mounts the part on a rotary table or faceplate (фланци, rings, discs, circular plates), while a Headstock Tailstock Positioner cradles a long part between driven and idler centers (валове, тръби, vessel shells). If the part is disc- or ring-shaped and mounts on a face, choose Single Axis Rotary; if it is long and spins about its own axis between centers, choose Headstock Tailstock.
Q: Can one welding positioner handle all geometries?
А: A Horizontal 3-Axis Rotary Positioner (the ROBOPTIX B008–B012 range) може, because it tilts, rotates, and adds a linear or secondary rotate axis to orient almost any contour. It is the most flexible family and the right choice when no simpler type fits—at a higher cost than a single-purpose unit, which is why geometry should drive the first cut.
Q: How do I verify a welding positioner’s accuracy before buying?
А: Ask the supplier to report pose accuracy AP and pose repeatability RP per ISO 9283:1998, с товар, температура, and speed stated—because the conditions are the number. ROBOPTIX is ISO 9001-certified and reports accuracy using ISO 9283:1998-подравнени показатели, and supports third-party or on-site laser-tracker verification with your part mounted and at temperature. A repeatability figure without those conditions is a half-truth.
A welding positioner for sale is a good buy only when the type fits the part. Start with geometry—Headstock Tailstock Positioner for long rotational work, Single Axis Rotary Positioner for flanges and rings, L-Type Welding Positioner for multi-face beams, U-Type Welding Positioner for large irregular frames, Horizontal 3-Axis Rotary Positioner for mixed seams, Vertical Tilting Positioner for heavy plate—then size on overturning moment and verify accuracy per ISO 9283:1998. ROBOPTIX е сертифициран по ISO 9001, covers all six families, and is typically priced 50–70% below overseas-brand equivalents while reporting accuracy on a comparable method. Send us your part drawing and duty cycle and we will spec the family, the moment rating, and the acceptance criteria—before you buy, не след.
Not sure which позиционер за заваряване type fits your part?
Изпратете РОБОПТИКС your part drawing and duty cycle for a free type-and-moment specification.
За автора
опит & пълномощията
Специалист по интегриране на роботизирана система за заваряване с 12+ години директен проектен опит, фокусиран върху избора и интегрирането на робот позиционер. Предоставя консултации на 300+ фабрики в цяла Северна Америка, Европа, и Азия. Всички спецификационни данни в тази статия са извлечени от действителните H / Б / Л / Продуктови листове с данни от серия U.
История на компанията: 26+ години инженеринг за автоматизация на заваряване, 40+ активни патенти, 1,500+ завършени проекти в световен мащаб, приблизително 70% включваща интеграция на Robot Positioner.
Сертификати
- ISO 9001: 2015 (GB/T 19001-2016) — Система за управление на качеството
- GJB 9001C-2017 — Система за управление на качеството на военно/оръжейно оборудване
- ЕС CE — Директива за машините 2006/42/ЕО (Серт. не. M.2026.206.C134866)
- Високотехнологично предприятие — Cert. не. GR202341000595 (Издадено ноем. 2023)
Последна актуализация: юни 2026
СВЪРЗАНИ ПУБЛИКАЦИИ

Планиране на автономна траектория в роботизирани заварчици:Какво означава това за вашата производствена линия

Контролен списък за закупуване на позиционер за заваряване: 6 Входящи данни за точен RFQ

Как да изберете доставчик на роботизирано лазерно заваряване: От техническа оценка до тестване на проби

Анатомия на роботизирана заваръчна клетка: Основни компоненти & Ръководство за избор (2026)

Монтаж & Ръководство за поддръжка на роботизирани системи за лазерно заваряване: Практическа пътна карта
