


Производитель индивидуальных роботизированных рабочих станций и лазерных систем



Аудит перед покупкой: Контрольный список посещения завода и протокол стендовых испытаний для покупателей сварочных позиционеров
Buying a сварочный позиционер is easy. Покупка подходящего сварочного позиционера у поставщика, которому можно доверять, не. Большинство решений о закупках основывается на сравнении технических характеристик., повторяемость, price—made across a table from three PDFs. That comparison misses the one thing that actually determines whether your cell works on day one: the supplier’s ability to build the machine to the spec, repeatedly, and to prove it. A pre-purchase audit—a structured factory visit plus a bench test of the actual welding positioner you are about to buy—closes that gap before money changes hands. This article gives you a factory-visit checklist and a bench-test protocol you can run yourself or mandate in the contract, so the welding positioner you specify is the welding positioner you receive.
An audit is not due-diligence theater. It is the same verification discipline from статья о проверке точности (Laser Tracker & ИСО 9283)—measure, don’t trust—applied one step earlier, to the vendor. A supplier whose welding positioners repeat to ±0.05 mm on the bench but cannot show you the calibration certificate, the machining tolerance on the faceplate, or a repeatable test procedure is a risk regardless of the number on the quote. The audit turns “they claim” into “we verified.”
Примечание: The audit protocol reflects РОБОПТИКС supplier-qualification and customer-acceptance practice, aligned with ISO 9283:1998 bench-test methodology (Можете ли вы доверять спецификации?? Проверка точности сварочного позиционера с помощью лазерных трекеров и ISO 9283) and the load/accuracy principles in this series. Связь между качеством сварки подтверждена рецензируемыми исследованиями. (Парк и др., 2019; Лю и др., 2023).
1. Why a Pre-Purchase Audit Beats a Spec-Sheet Comparison
A spec sheet is a promise written by the seller. Two suppliers can quote the identical “±0.05 mm repeatability, 2,000 kg” welding positioner at different prices, and only one may be able to deliver it. The difference lives in things the PDF never shows: how the faceplate is machined, whether the gearbox is graded, how the controller is tuned, and whether anyone actually tests the finished machine. An audit is how you see those things. It also shifts leverage: a supplier who knows you will bench-test the welding positioner at their factory is incentivized to show you the real number, not the marketing number. For an international buyer paying in advance and waiting weeks for ocean freight, that leverage is worth more than any single line item on the quote.
2. The Factory Visit Checklist
A factory visit is only useful if you know what to look for. Walk the floor with a checklist, not a tour guide. The items below separate suppliers who build welding positioners to a process from those who assemble them to an order.
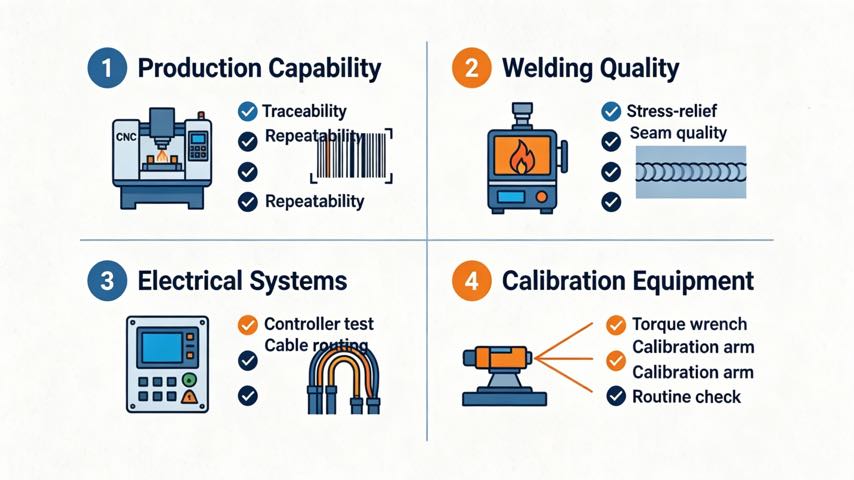
2.1 Production Capability & Прослеживаемость
- Machine capability: Can they show you the CNC machining of a positioner bed or faceplate in progress, with tolerances documented? A welding positioner is only as accurate as the surface your part bolts to, and that surface starts at the machine datum.
- Прослеживаемость: Are major components—gearbox, подшипники, servo motors, controller—batch- and serial-tracked? If a welding positioner fails in year two, can they tell you exactly what went into it?
- Build routine: Do they build this class of welding positioner routinely, or is your order a one-off outside their norm? Routine builds mean routine, repeatable quality; one-offs mean learning on your dime.
2.2 Сварка & Machining Quality
- Frame integrity: Is the structural frame stress-relieved after welding? A frame that is not stress-relieved can twist after you mount it, destroying the accuracy you paid for. Ask to see the stress-relief records.
- Weld finish: Последовательный, slag-free welds with proper post-weld treatment signal process control. Sloppy frame welds predict a sloppy welding positioner.
- Datum control: Are reference datums protected and re-checked? The calibration chain (Можете ли вы доверять спецификации?? Проверка точности сварочного позиционера с помощью лазерных трекеров и ISO 9283) starts at the machine datum, and a damaged datum corrupts every measurement downstream.
2.3 Электрический & Control Systems
- Controller transparency: Is the control system a recognized brand with support, or a black box? You will need to integrate it with your robot (Программирование координированного движения: Робот и позиционер как одна кинематическая цепь); a black-box controller is a future integration wall.
- Cabling and dress packs: Are cables routed and strain-relieved for the duty you specified, or minimally? Cable drag is a real, measurable field error source ((Можете ли вы доверять спецификации?? Проверка точности сварочного позиционера с помощью лазерных трекеров и ISO 9283)) and a common cause of intermittent accuracy loss.
2.4 Калибровка & Test Equipment
- Metrology ownership: Do they own a laser tracker or calibrated metrology to accept the welding positioner, or do they “eyeball” repeatability? A supplier who cannot measure a welding positioner cannot guarantee one ((Можете ли вы доверять спецификации?? Проверка точности сварочного позиционера с помощью лазерных трекеров и ISO 9283)).
- Test fixtures: Are load weights and fixturing available to demonstrate your actual part, not a token mass? If they can only test empty, they can only promise empty.
3. The Bench Test Protocol
The bench test is where the audit becomes evidence. You are not inspecting; you are measuring the specific welding positioner offered to you, against a written procedure, before you pay. A witnessed bench test with your part mounted is the single most decisive step in supplier qualification.
3.1 What to Measure
Measure against ISO 9283:1998 (Можете ли вы доверять спецификации?? Проверка точности сварочного позиционера с помощью лазерных трекеров и ISO 9283): pose repeatability RP and pose accuracy AP at minimum, plus drift over a sustained run. Record the conditions—temperature, нагрузка, speed—because, as showed, the conditions are the number. For a welding positioner you will load, add a loaded and at-temperature run, not just the empty cold test; that is where load sag and thermal drift (the hidden specs from the hidden-specs article reveal themselves.
3.2 The Test Procedure
- 1. Witness, don’t receive: Be present, or hire a third-party inspector, when the welding positioner is tested. A video of someone else’s test is not your test, and it is trivially easy to shows the best of ten runs.
- 2. Use your part or a representative mass: Test with the actual production part or a mass and center-of-gravity matching it (Эксцентричная нагрузка & Опрокидывающий момент: Почему 2-тонный сварочный позиционер не справляется с 2-тонной деталью); empty-bed numbers hide load sag and backlash (the hidden-specs article).
- 3. Run the full pose grid: Sweep the working envelope—tilt and rotate through the range you will actually use—with ten repetitions per pose, at your operating temperature and speed.
- 4. Log drift: Run a continuous duty cycle for 2–4 hours and re-measure; ИСО 9283 drift separates a machine that is good cold from one that stays good hot.
- 5. Get the raw report: Demand the data—poses, readings, температура, σ band—not a summary bullet. The report is what you hold the supplier to, and what survives a dispute.
3.3 Accept/Reject Criteria
Your acceptance criteria should already be in the purchase order as a clause ((Можете ли вы доверять спецификации?? Проверка точности сварочного позиционера с помощью лазерных трекеров и ISO 9283)): например, “welding positioner RP ≤ 0.05 mm and AP ≤ 0.10 mm per ISO 9283, в [температура]/[нагрузка]/[скорость], ±2σ, laser-tracked.” The bench test is simply the moment that clause is enforced. If the welding positioner fails, you have a documented, contractual reason to reject or rework—before it ships, not after it is in your cell.
| Test | What it proves | Acceptance reference |
| Empty-bed repeatability (РП) | Axis repeats as quoted, unloaded and cold | ИСО 9283 РП, ±2σ |
| Loaded accuracy (АП) | Holds pose with your part mounted | ИСО 9283 АП; your PO clause |
| Drift over 2–4 h | Stays accurate hot, under duty | ИСО 9283 дрейфовать |
| Люфт / stiffness spot-check | Hidden specs (the hidden-specs article) within class | Supplier spec + the hidden-specs article method |
| Coordinated motion (if robot cell) | Moves as external axis, no sync loss | EtherCAT sync test |
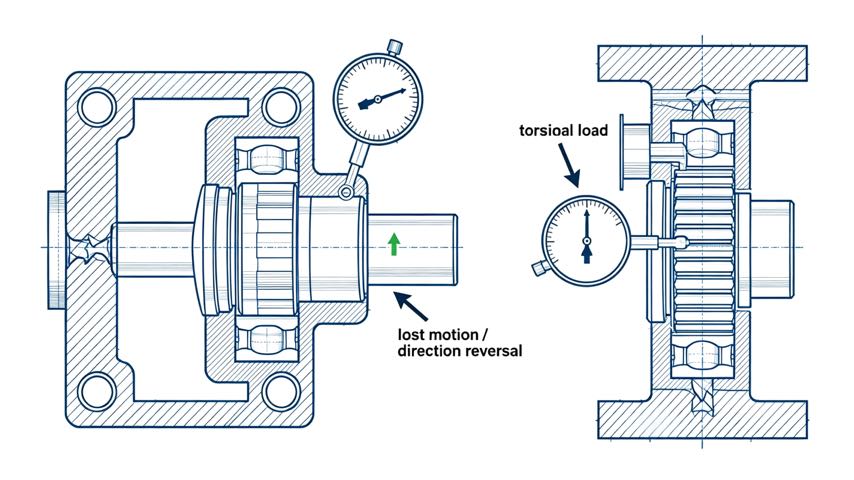
4. Verifying the Hidden Specs
The bench test should also probe the hidden specs the hidden-specs article taught us to care about: обратная реакция, крутильная жесткость, и тепловой дрейф. А сварочный позиционер can show good repeatability yet have sloppy backlash that appears as seam inconsistency at direction changes, or low stiffness that lets a heavy part deflect mid-weld. Ask the supplier to demonstrate—or let you measure—backlash at a reversal and stiffness under a side load. These are the numbers serious buyers check and casual ones regret. If the supplier has no method to show them, это отсутствие само по себе является ответом, and it tells you how much of their spec sheet is measurement versus assumption.
5. Red Flags: What Makes You Walk Away
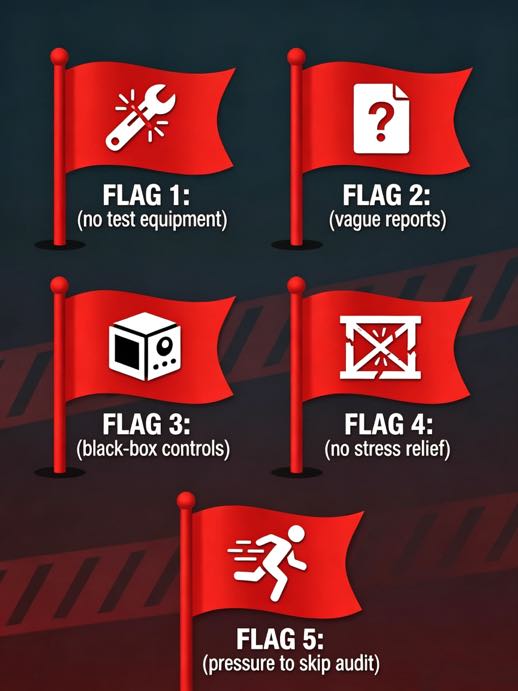
- No test equipment: If they cannot measure a welding positioner to the spec they quote, the spec is aspirational, not assured.
- Vague or missing reports: Promises without raw data, or “we don’t usually test that.” A claim with no report is a claim, не доказательство.
- Black-box controls: A controller you cannot integrate with your robot (Программирование координированного движения: Робот и позиционер как одна кинематическая цепь) or get support for will cost you later.
- No stress relief or datum control: A frame that will drift after you mount it, quietly wrecking accuracy.
- Pressure to skip the audit: Any resistance to witnessing the bench test is itself the strongest red flag—it signals they expect the test to disappoint you.
6. Пример поля: The Audit That Saved a Bad Order
A ROBOPTIX customer was about to commit to a low-cost welding positioner from a new supplier. The quote looked strong on paper—±0.04 mm, attractive price. We ran a pre-purchase audit. The factory visit revealed they owned no laser tracker (they measured repeatability with a dial gauge on a short arm, which under-resolves angular error by roughly an order of magnitude), performed no stress relief on frames, and offered a controller they could not integrate with the customer’s robot brand. Their bench “test” was a single cold, empty run. The customer walked away and instead specified a ROBOPTIX сварочный позиционер with an ISO 9283 laser-tracker acceptance built into the purchase order. The audit cost one site visit; it prevented a misintegrated cell and a likely rejected shipment. The cheap quote was, as it turned out, the expensive one.
7. When a Full Audit Isn’t Needed
A full factory audit and witnessed bench test are not free, and not every purchase warrants them. If you are reordering a proven welding positioner from a qualified, previously audited supplier, a certificate of conformance may suffice. If the part tolerance is loose (±1 мм) and the welding positioner is a standard, catalog unit you have run before, a paper audit—reviewing the ISO 9283 report and component traceability—is enough. Reserve the full on-site audit for first-time suppliers, жесткие допуски (±0,2 мм и ниже), тяжелые или нестандартные детали (Круглый, прямоугольный и неправильный: Согласование конфигурации сварочного позиционера с геометрией заготовки), or any welding positioner you will integrate into a coordinated cell (Программирование координированного движения: Робот и позиционер как одна кинематическая цепь). Spend the audit where the risk lives; skip it where you already have the evidence. Решение, не ритуальный, is what protects the budget.
Часто задаваемые вопросы
вопрос: What should I check when visiting a welding positioner factory?
А: Verify they can machine and document the faceplate datum, track major components for traceability, stress-relieve frames, and—critically—own calibrated metrology such as a laser tracker to actually measure repeatability and accuracy. A supplier who cannot measure a welding positioner cannot guarantee one, no matter how confident the quote sounds.
вопрос: How do I bench-test a welding positioner before buying?
А: Witness the test (or use a third-party inspector), measure against ISO 9283 with your actual part or a matching mass mounted, sweep the full pose grid with ten repeats per pose at your operating temperature and speed, log drift over 2–4 hours, and demand the raw data report. Then enforce the acceptance criteria already written into your purchase order.
вопрос: Why verify backlash and stiffness, not just repeatability?
А: A welding positioner can repeat well yet have sloppy backlash that shows up as seam inconsistency at direction changes, or low stiffness that lets a heavy part deflect mid-weld. These hidden specs (the hidden-specs article) decide real-world weld quality even when the headline repeatability looks fine, which is why a serious audit checks them.
вопрос: Do I always need a full factory audit?
А: Нет. Reorders from a previously audited supplier, loose-tolerance standard units, or parts you have run before may only need a paper audit—reviewing the ISO 9283 report and traceability. Reserve the full on-site audit for first-time suppliers, жесткие допуски, тяжелые или нестандартные детали, or coordinated robot cells, where the risk justifies the cost.
Заключение
A spec-sheet comparison tells you what a supplier claims; a pre-purchase audit tells you what they can prove. Visit the factory with a checklist, bench-test the actual welding positioner against ISO 9283 with your part mounted and at temperature, verify the hidden specs, and write the acceptance criteria into the purchase order before you pay. The audit is the same measurement discipline that makes a welding positioner work on your floor—applied one step upstream, to the vendor. Сделай это один раз, on the order that matters, and you stop buying promises and start buying proof.
РОБОПТИКС welding positioners ship against ISO 9283-referenced, laser-tracked acceptance reports and support customer and third-party audits, including witnessed bench tests with your production part. For a first-time supplier decision, that transparency is the difference between a cell that works on day one and a shipment you argue about for months. The next and final article (P10) puts a number on the whole decision: the five-year total cost of ownership of a welding positioner, and why the cheap quote is often the expensive one.
Specifying a welding positioner from a new supplier?
Просить РОБОПТИКС for an auditable, ИСО 9283 laser-tracked acceptance plan written into your purchase order.
Об авторе
Опыт & Реквизиты для входа
Специалист по интеграции роботизированных сварочных систем с 12+ многолетний опыт реализации проектов, направленный на выбор и интеграцию позиционера робота. Оказывал консультации 300+ заводы по всей Северной Америке, Европа, и Азия. Все технические данные в этой статье взяты из фактического H. / Б / л / Технические характеристики продукции серии U.
История компании: 26+ лет разработки в области автоматизации сварки, 40+ действующие патенты, 1,500+ реализованные проекты по всему миру, примерно 70% включая интеграцию позиционера робота.
Сертификаты
- ИСО 9001: 2015 (ГБ/Т 19001-2016) — Система менеджмента качества
- GJB 9001C-2017 — Система управления качеством военной/оружейной техники
- ЕС CE — Директива по машинному оборудованию 2006/42/EC (Сертификат. Нет. М.2026.206.C134866)
- Высокотехнологичное предприятие — Сертификат. Нет. ГР202341000595 (Выпущено в ноябре. 2023)
Ссылки
[1] Международная организация по стандартизации. (1998). ИСО 9283:1998, Управление промышленными роботами. Критерии производительности и соответствующие методы испытаний.
[2] Парк, Ж.-Х., Ким, С.-Х., Луна, Х.-С., & Ким, М.-Х. (2019). Влияние силы тяжести на поведение ванны расплава и анализ микроструктуры в различных положениях сварки при дуговой сварке металлов в импульсном газе.Прикладные науки, 9(21), 4626.
[3] Лю, Дж., Цзян, Ф., Чен, С., Сюй, Б., Чжан, Г., Ченг, В., & Ма, Х. (2023). Механизмы гравитационного влияния на поведение сварочной ванны и характеристики сварного шва при плазменно-дуговой сварке переменной полярности в различных сварочных положениях.Материалы, 16(19), 6457.
ПОХОЖИЕ ПОСТЫ

Ручная и роботизированная сварка конструкционной стали:Когда автоматизация окупается?

1От G до 6G без крана: Как позиционер преобразует верхние сварные швы в плоские сварные швы

Как установить и интегрировать робота 7-й оси: Пошаговое руководство & Лучшие практики
Сколько стоит роботизированная сварочная камера? 2026? Полная разбивка цен

Установка & Руководство по техническому обслуживанию роботизированных систем лазерной сварки: Практическая дорожная карта
