


Производитель индивидуальных роботизированных рабочих станций и лазерных систем



6 Общие проблемы роботизированной лазерной сварки и способы их решения
В предыдущих статьях, мы исследовали революционные преимущества роботизированной лазерной сварки в автомобильной легкой промышленности.. Однако, как высокоточный процесс, the implementation of laser welding in actual factory environments is not always smooth sailing. Due to the extremely small laser spot size and rapid cooling rate, even the slightest process deviation can lead to welding defects. Facing challenges head-on is a sign of a maturing technology. Сегодня, we will delve into the six major challenges commonly encountered in robotic laser welding during production and share industry-proven solutions.
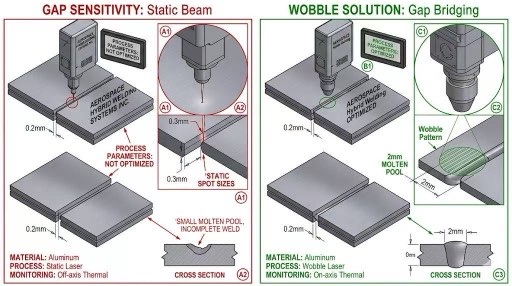
1. Extreme Sensitivity to Assembly Gaps (Gap Sensitivity)
Испытание: The laser spot diameter is typically only 0.2–0.6 mm. If the assembly gap between parts exceeds 0.1 мм, the laser beam may pass directly through the gap, resulting in “missed welds” or severe collapse. This places extremely high demands on the stamping precision of preceding processes.
Решения:
Laser Wobbling Welding Technology: By integrating high-frequency vibrating mirrors into the welding head, the spot is made to oscillate rapidly in a circular or figure-eight pattern. This not only widens the molten pool but also significantly improves tolerance for assembly gaps.
Wire Feed Welding: Automatically feeds welding wire into areas with larger gaps, ensuring a full weld bead through the addition of filler metal.
2. Welding Spatter and Surface Contamination (Spatter Control)
Испытание: When welding high-strength steel or galvanized steel, violent fluctuations in the molten pool and metal vapor can cause liquid metal spatter. This not only damages the aesthetic appearance of the workpiece surface but also contaminates precision laser lenses.
Решения:
Beam Shaping: Utilizing ring-spot technology (adjustable ring-core lasers), the outer ring preheats the molten pool while the inner ring performs deep penetration welding, resulting in a smoother welding process.
Optimized Shielding Gas Flow: A dedicated shielding gas device (lateral gas flow) is designed to protect the lens with a stable gas curtain and remove metal vapors.
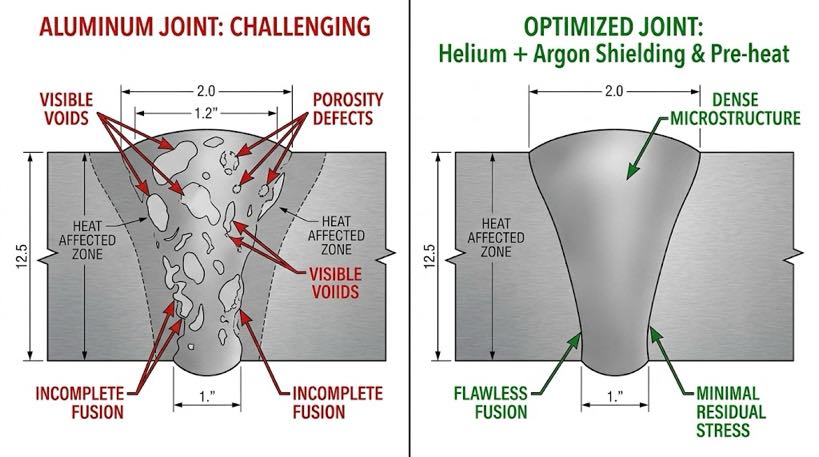
3. Porosity in Aluminum Welding
Испытание: Aluminum alloys have extremely high hydrogen solubility, and the laser weld pool solidifies very rapidly, preventing hydrogen from escaping in time. This results in the formation of numerous pores within the weld, severely compromising structural strength.
Решения:
Surface Pre-treatment: Strictly perform chemical cleaning or mechanical grinding prior to welding to remove surface oxide layers and residual oils.
Dual-Spot Welding: Utilize two laser spots working in tandem to extend the duration of the molten pool, providing a “lifeline” for gas bubbles to escape.
4. Focus Shift Affecting Consistency
Испытание: During high-power continuous welding, the optical components of the welding head can deform due to heat absorption from a small amount of energy, causing the focal point to shift and resulting in fluctuations in weld depth.
Решения:
Total Reflection Optical Design: Select high-quality, low-absorption lenses or replace transmissive lenses with total reflection mirrors.
Real-Time Focus Compensation System: Monitor lens temperature via sensors and automatically adjust the robot end-effector height to ensure the focus remains locked onto the workpiece surface.
5. Risk of Damage from Highly Reflective Materials (Back Reflection)
Испытание: When welding highly reflective metals such as copper and aluminum, the laser beam may reflect back into the fiber like a mirror, damaging the expensive laser source.
Решения:
Anti-reflection isolation technology: Equip the laser with multi-stage anti-reflection devices that shut down the laser within milliseconds upon detecting reflected light.
Tilted welding angle: Tilt the laser head at an angle of 5°–10° to divert reflected light away from the laser output port.
6. Lack of In-line Quality Monitoring
Испытание: Laser welding speeds are extremely high (до 10 м/мин). Traditional post-welding visual inspection cannot detect internal defects in a timely manner, leading to a large number of defective parts.
Решение:
Multi-spectral optical monitoring: Utilizes visual and infrared sensors to capture plasma light signals emitted by the molten pool in real time, automatically identifying defects such as porosity and lack of fusion through AI algorithms.
Optical Coherence Tomography (OCT): Measures weld depth in real time using coherent light while welding.
Роботизированная лазерная сварка: A Comparison of Technology Maturity
| Challenge Dimension | Текущий статус | Solution Maturity | Key Considerations |
| Gap Sensitivity | Significantly Mitigated | Высокий (Pendulum welding technology is widely adopted) | Precision of fixtures in preceding processes |
| Spatter Control | Controllable | Умеренный (Requires optimization for specific materials) | Application of Adjustable Ring-Core Laser Sources |
| Aluminum Alloy Porosity | Effectively Reduced | Середина | Pre-welding cleaning process management |
| High Reflectivity | Extremely Low Risk | Extremely High (Hardware protection is already well-established) | Welding head tilt angle settings |
Robotic laser welding is not a simple “plug-and-play” technology; it does indeed present numerous challenges. Однако, with the widespread adoption of oscillating welding, spot-by-spot technology, and in-line inspection systems, standardized solutions now exist for these once-daunting challenges. Mastering these best practices is key for companies to transition from “being able to weld” to achieving “high-quality welding.”
Следующая статья Предварительный просмотр: «Why Does Robotic Laser Welding Need a Vision System? From Blind Welding to Intelligent Welding»
Идентификация автора
Эксперт в области интеграции систем роботизированной сварки с более чем 12 многолетний опыт работы в отрасли. Моя компания закончила 26 лет профессионального опыта, держит больше, чем 40 запатентованные технологии, и успешно завершил более 1,500 проекты по всему миру (примерно 70% из них задействованы роботизированные сварочные ячейки, на общую сумму более 1,000 единицы). Компания имеет сертификат ЕС CE. (Сертификат №.: М.2026.206.C134866) и соответствует EN 60204-1:2018 и EN ISO 12100:2010 стандарты. Я помогал многочисленным производственным компаниям на протяжении всего процесса внедрения роботизированной сварочной станции., от отбора до запуска производства.
Обновлено: Может 2026
ПОХОЖИЕ ПОСТЫ

Сравнение типов сварочных позиционеров: передняя бабка, L-тип, U-тип, 3-Ось & Более

2026 7Руководство по выбору робота оси: Полезная нагрузка, Гладить, Повторяемость & Совместимость брендов

Роботизированная сварочная камера в сравнении с традиционной сварочной линией: Что на самом деле меняется в вашем цехе

Расчет полезной нагрузки позиционера робота и безопасный выбор: Полное инженерное руководство

Лазерный сварочный позиционер: Точность и скорость сварных швов тонкой толщины
