Custom Robot Workstations And Laser Systems Manufacturer



6 Common Challenges in Robotic Laser Welding and How to Solve Them
In previous articles, we explored the revolutionary advantages of robotic laser welding in automotive lightweighting. However, as a highly precise process, the implementation of laser welding in actual factory environments is not always smooth sailing. Due to the extremely small laser spot size and rapid cooling rate, even the slightest process deviation can lead to welding defects. Facing challenges head-on is a sign of a maturing technology. Today, we will delve into the six major challenges commonly encountered in robotic laser welding during production and share industry-proven solutions.
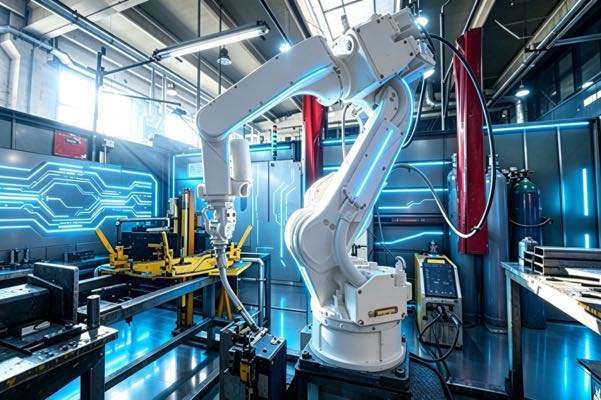
1. Extreme Sensitivity to Assembly Gaps (Gap Sensitivity)
Challenge: The laser spot diameter is typically only 0.2–0.6 mm. If the assembly gap between parts exceeds 0.1 mm, the laser beam may pass directly through the gap, resulting in “missed welds” or severe collapse. This places extremely high demands on the stamping precision of preceding processes.
Solutions:
Laser Wobbling Welding Technology: By integrating high-frequency vibrating mirrors into the welding head, the spot is made to oscillate rapidly in a circular or figure-eight pattern. This not only widens the molten pool but also significantly improves tolerance for assembly gaps.
Wire Feed Welding: Automatically feeds welding wire into areas with larger gaps, ensuring a full weld bead through the addition of filler metal.
2. Welding Spatter and Surface Contamination (Spatter Control)
Challenge: When welding high-strength steel or galvanized steel, violent fluctuations in the molten pool and metal vapor can cause liquid metal spatter. This not only damages the aesthetic appearance of the workpiece surface but also contaminates precision laser lenses.
Solutions:
Beam Shaping: Utilizing ring-spot technology (adjustable ring-core lasers), the outer ring preheats the molten pool while the inner ring performs deep penetration welding, resulting in a smoother welding process.
Optimized Shielding Gas Flow: A dedicated shielding gas device (lateral gas flow) is designed to protect the lens with a stable gas curtain and remove metal vapors.
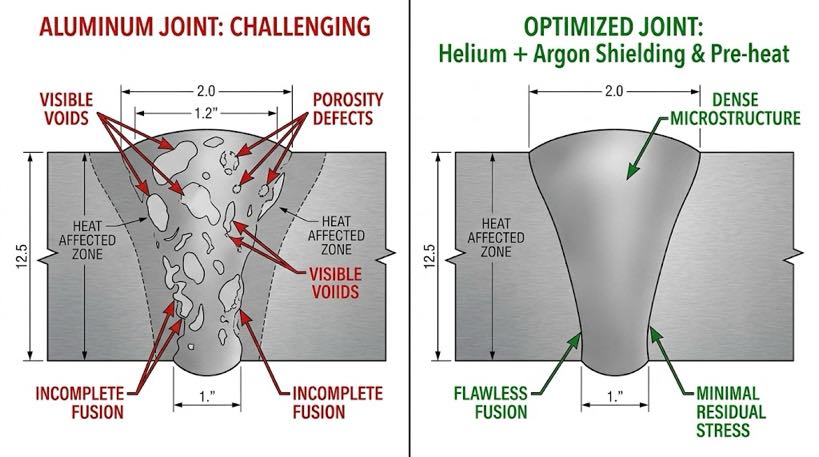
3. Porosity in Aluminum Welding
Challenge: Aluminum alloys have extremely high hydrogen solubility, and the laser weld pool solidifies very rapidly, preventing hydrogen from escaping in time. This results in the formation of numerous pores within the weld, severely compromising structural strength.
Solutions:
Surface Pre-treatment: Strictly perform chemical cleaning or mechanical grinding prior to welding to remove surface oxide layers and residual oils.
Dual-Spot Welding: Utilize two laser spots working in tandem to extend the duration of the molten pool, providing a “lifeline” for gas bubbles to escape.
4. Focus Shift Affecting Consistency
Challenge: During high-power continuous welding, the optical components of the welding head can deform due to heat absorption from a small amount of energy, causing the focal point to shift and resulting in fluctuations in weld depth.
Solutions:
Total Reflection Optical Design: Select high-quality, low-absorption lenses or replace transmissive lenses with total reflection mirrors.
Real-Time Focus Compensation System: Monitor lens temperature via sensors and automatically adjust the robot end-effector height to ensure the focus remains locked onto the workpiece surface.
5. Risk of Damage from Highly Reflective Materials (Back Reflection)
Challenge: When welding highly reflective metals such as copper and aluminum, the laser beam may reflect back into the fiber like a mirror, damaging the expensive laser source.
Solutions:
Anti-reflection isolation technology: Equip the laser with multi-stage anti-reflection devices that shut down the laser within milliseconds upon detecting reflected light.
Tilted welding angle: Tilt the laser head at an angle of 5°–10° to divert reflected light away from the laser output port.
6. Lack of In-line Quality Monitoring
Challenge: Laser welding speeds are extremely high (up to 10 m/min). Traditional post-welding visual inspection cannot detect internal defects in a timely manner, leading to a large number of defective parts.
Solution:
Multi-spectral optical monitoring: Utilizes visual and infrared sensors to capture plasma light signals emitted by the molten pool in real time, automatically identifying defects such as porosity and lack of fusion through AI algorithms.
Optical Coherence Tomography (OCT): Measures weld depth in real time using coherent light while welding.
Robotic Laser Welding: A Comparison of Technology Maturity
| Challenge Dimension | Current Status | Solution Maturity | Key Considerations |
| Gap Sensitivity | Significantly Mitigated | High (Pendulum welding technology is widely adopted) | Precision of fixtures in preceding processes |
| Spatter Control | Controllable | Moderate (Requires optimization for specific materials) | Application of Adjustable Ring-Core Laser Sources |
| Aluminum Alloy Porosity | Effectively Reduced | Medium | Pre-welding cleaning process management |
| High Reflectivity | Extremely Low Risk | Extremely High (Hardware protection is already well-established) | Welding head tilt angle settings |
Robotic laser welding is not a simple “plug-and-play” technology; it does indeed present numerous challenges. However, with the widespread adoption of oscillating welding, spot-by-spot technology, and in-line inspection systems, standardized solutions now exist for these once-daunting challenges. Mastering these best practices is key for companies to transition from “being able to weld” to achieving “high-quality welding.”
Next Article Preview: “Why Does Robotic Laser Welding Need a Vision System? From Blind Welding to Intelligent Welding”
Author Identification
An expert in robotic welding system integration with over 12 years of industry experience. My company has over 26 years of professional experience, holds more than 40 patented technologies, and has successfully completed over 1,500 projects worldwide (approximately 70% of which involved robotic welding cells, totaling more than 1,000 units). The company holds EU CE certification (Certificate No.: M.2026.206.C134866) and complies with the EN 60204-1:2018 and EN ISO 12100:2010 standards. I have assisted numerous manufacturing companies throughout the entire process of robotic welding workstation implementation, from selection to production launch.
Updated: May 2026
RELATED POSTS
Robotic Welding Cell vs Manual Welding: Which Is Better for Modern Manufacturing?

7th Axis Robot Track System Maintenance & Troubleshooting Guide
Coordinated Motion Programming: Making Your Robot and Positioner Move as One Kinematic Chain
Welding Positioner Types Compared: Headstock, L-Type, U-Type, 3-Axis & More

Scan-to-Weld Technology:How Reverse Modeling Replaces Robot Programming