Custom Robot Workstations And Laser Systems Manufacturer



Robotic Laser Welding: Principles, Advantages, and Applications (2026 Complete Guide)
Introduction
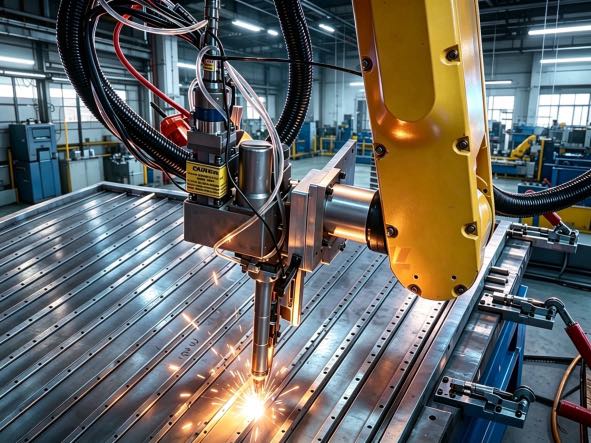
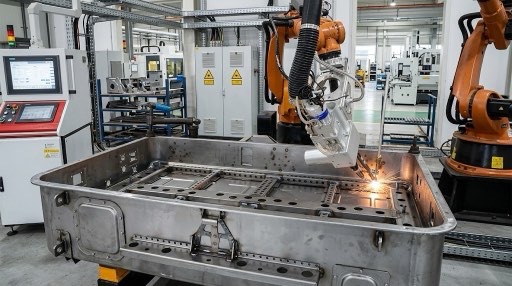
Robotic laser welding has become the most competitive automated welding process in modern manufacturing. It combines high-energy-density laser beams with multi-axis industrial robots to achieve high-speed, high-precision, non-contact welding of metal components.
According to Global Market Insights, the global robotic laser welding market exceeded $1.7 billion in 2025, is projected to reach $1.9 billion in 2026, and is expected to approach $4 billion by 2035, with a compound annual growth rate (CAGR) of approximately 8.9%. New energy vehicles, power batteries, and precision manufacturing primarily drive this growth.
Whether you are in the automotive, power battery, medical device, or consumer electronics industry, understanding its principles, advantages, and limitations is key to evaluating its investment value.
Data Sources: This article is based on the latest technical documentation from suppliers such as IPG Photonics, TRUMPF, and Fanuc, as well as on-site feedback from multiple Tier 1 suppliers and battery manufacturers. All data is publicly verifiable.
Working Principle
The core of robotic laser welding lies in highly efficient energy conversion: electrical energy is converted into a laser beam, which is then focused onto the metal surface to instantly melt and solidify it, forming a weld. The process is non-contact and results in a minimal heat-affected zone.
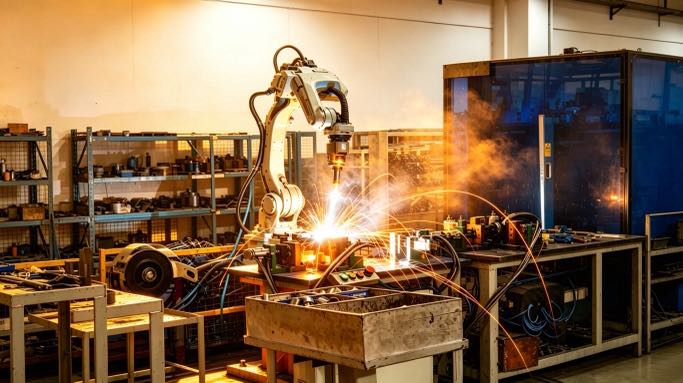
The welding process consists of four steps:
1. Laser Generation: Fiber lasers are the mainstream choice, operating at a wavelength of approximately 1070 nm and power ranging from 500 W to over 6 kW. Raycus、MAX Photonics fiber lasers achieve an electro-optical conversion efficiency of over 40%, with the ECO series exceeding 35%, far surpassing traditional CO₂ lasers (approximately 10%). They are energy-efficient and stable.
2. Beam Transmission: The laser is transmitted through a 50-200 μm fiber optic cable to the robotic welding head, with virtually no energy loss and no impact from joint movement.
3. Focusing and Positioning: The welding head focuses the beam into a 0.2–0.8 mm spot with an energy density as high as 10⁶–10⁷ W/cm², capable of melting metal in milliseconds. 6-axis robots achieve repeatability of ±0.05 mm (Fanuc, KUKA, ABB, etc.).
4. Melt Pool Formation and Solidification: The laser creates a “keyhole” effect, generating a vapor channel within the metal surrounded by a liquid melt pool. Heating and cooling rates are extremely fast (10³–10⁶ °C/s), with a heat-affected zone of only 0.1–1 mm.
Technical Highlights: Supports self-fusion welding without the need for filler wire, eliminating the risk of material composition inconsistencies.
Core Components and Configuration Options
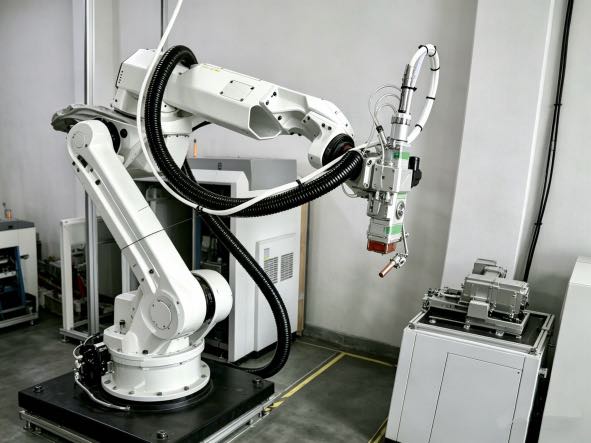
Industrial-grade systems consist of five core modules:
| Component | Function | Typical Specifications | Selection Criteria |
| Laser | Generates laser energy | Fiber laser, 1–6 kW+ | Select power based on material thickness and speed |
| Industrial Robot | Executes motion paths | 6-axis, payload 10–50 kg | Covers the total weight of the welding head and cables |
| Laser Welding Head | Focuses the beam | Collimating lens 100/150 mm, focusing lens 150–300 mm | Long focal length suitable for deep cavities; short focal length suitable for high speeds |
| Control System | Coordinates movements | PLC + Dedicated software | Supports real-time power modulation |
| Safety Protection(Optional) | Laser protection | Class 4 safety enclosure + Interlocks | Complies with IEC 60825-1 standard |
Optional high-end configurations: Vision-based weld seam tracking (±0.1 mm), OCT online penetration depth monitoring, and oscillating welding head (to reduce gap sensitivity).
Key Application Scenarios and Case Studies
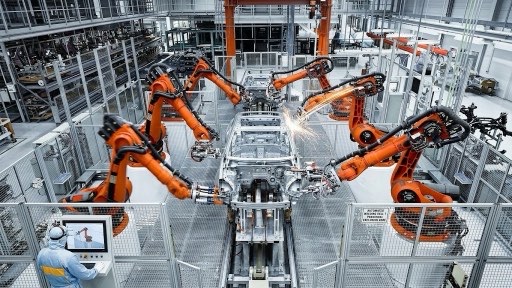
1. Automotive Manufacturing: White body side panels, doors, B-pillars, etc. Materials include galvanized steel, hot-formed boron steel, and 6000-series aluminum. A European luxury automaker has deployed multiple systems on its electric vehicle platform, achieving a welding speed of 90 mm/s and an annual production capacity exceeding 100,000 units.
2. Power Batteries: Busbars, tabs, and pressure relief valves. Materials include red copper, aluminum, and copper-aluminum dissimilar metals. A leading battery manufacturer has deployed over 200 systems, with a single-line capacity of 200 ppm and a defect rate below 0.3%.
3. Medical Devices: Pacemaker housings, surgical instruments. Materials include Ti6Al4V and 316L stainless steel. Welds are contamination-free, rework rates have dropped from 4.2% to 0.6%, and the process is ISO 13485 certified.
4. Consumer Electronics: Smartphone mid-frames, headphone contacts. Weld width: 0.3 mm; aesthetically pleasing with a small heat-affected zone, allowing for anodizing without grinding.
Clarification of Common Misconceptions
Q1: Is robotic laser welding limited to thin sheets?
Q2: Does robotic laser welding have to be performed in a dust-free environment (cleanroom)?
Q3: Robotic laser welding equipment is extremely expensive—can small factories afford it?
Q4: Is robotic laser welding very complex to operate, requiring professional welding engineers?
Q5: Does laser welding require any shielding gas?
FAQ
Q1: How fast is the welding speed? Typical data: 1 mm stainless steel at 80–120 mm/s (1 kW); 2 mm aluminum alloy: 40–60 mm/s (2 kW); 0.3 mm copper foil: 150–200 mm/s (pulsed mode). Actual speeds require optimization based on material and power.
Q2: What is the approximate initial investment? An entry-level complete system (1 kW laser + small 6-axis robot + welding head + safety enclosure) costs approximately $30,000–$80,000.
Q3: Is it difficult to learn? Operator training typically takes 1–2 weeks and covers offline programming, laser safety, and parameter adjustment. Basic knowledge of metals is sufficient; no background as a professional welding engineer is required.
Q4: Is the weld strength lower than that of MIG welding? The strength of self-fusion laser welds typically reaches 90%–100% of the base material. When there is a gap, strength can be enhanced through oscillating welding or wire-fed laser welding.
Q5: Which safety standards are met? These primarily include IEC 60825-1 (Safety of laser products) and ISO 11553 (Safety of laser processing machines). The equipment must be equipped with a Class 4 safety enclosure, interlock switches, and emergency stop devices.
References
IPG Photonics Fiber Laser Welding Guide
TRUMPF Automotive Laser Welding
Global Market Insights Robotics Laser Welding Report
IEC 60825-1:2014
Disclaimer: The information in this article is for reference only; actual results require verification through sample testing.
Author Identification
This article is based on the International Federation of Robotics (IFR) World Robotics Report 2025, American Welding Society (AWS) workforce data, and major manufacturer technology roadmaps.
Author:
An expert in robotic welding system integration with over 12 years of industry experience. My company has over 26 years of professional experience, holds more than 40 patented technologies, and has successfully completed over 1,500 projects worldwide (approximately 70% of which involved robotic welding cells, totaling more than 1,000 units). The company holds EU CE certification (Certificate No.: M.2026.206.C134866) and complies with the EN 60204-1:2018 and EN ISO 12100:2010 standards. I have assisted numerous manufacturing companies throughout the entire process of robotic welding workstation implementation, from selection to production launch.
Updated: May 2026
RELATED POSTS
8 Costly Mistakes When Deploying a Robotic Welding Cell (And How to Avoid Them) – 2026 Edition

How to Integrate a Vision-Guided Robotic Welding cell into an Existing Fabrication Line

Robotic Welding Cell Maintenance Guide: Best Practices, Schedule & Troubleshooting 2026
What Is a Robotic Welding Cell? 2026 Beginner’s Guide | 37 Shop Data
Head-and-Tailstock vs. L-Type vs. U-Type Robot Positioner: How to Choose by Workpiece Shape