


Fabricante de sistemas láser y estaciones de trabajo robóticas personalizadas



Soldadura láser robótica: Principios, Ventajas, y aplicaciones (2026 Guía completa)
Introduction
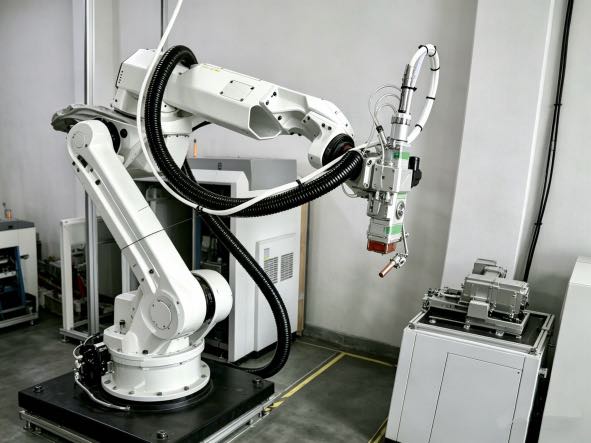
Robotic laser welding has become the most competitive automated welding process in modern manufacturing. Combina rayos láser de alta densidad de energía con robots industriales multieje para lograr alta velocidad., alta precisión, non-contact welding of metal components.
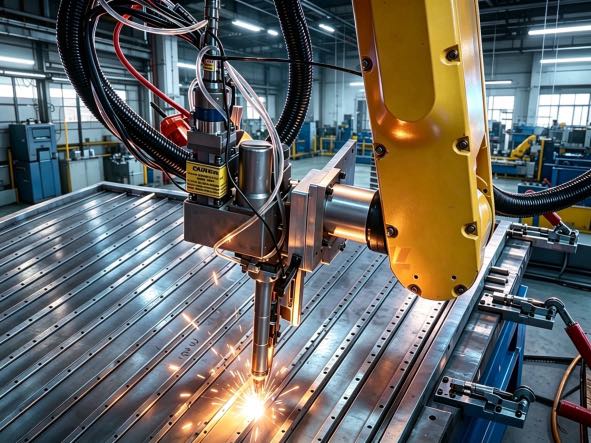
De acuerdo a Global Market Insights, the global robotic laser welding market exceeded $1.7 billion in 2025, is projected to reach $1.9 billion in 2026, and is expected to approach $4 mil millones por 2035, with a compound annual growth rate (CAGR) of approximately 8.9%. New energy vehicles, power batteries, and precision manufacturing primarily drive this growth.
Whether you are in the automotive, power battery, dispositivo medico, or consumer electronics industry, understanding its principles, advantages, and limitations is key to evaluating its investment value.
Fuentes de datos: This article is based on the latest technical documentation from suppliers such as IPG Photonics, TRUMPF, and Fanuc, as well as on-site feedback from multiple Tier 1 suppliers and battery manufacturers. All data is publicly verifiable.
Working Principle
The core of robotic laser welding lies in highly efficient energy conversion: electrical energy is converted into a laser beam, which is then focused onto the metal surface to instantly melt and solidify it, forming a weld. The process is non-contact and results in a minimal heat-affected zone.
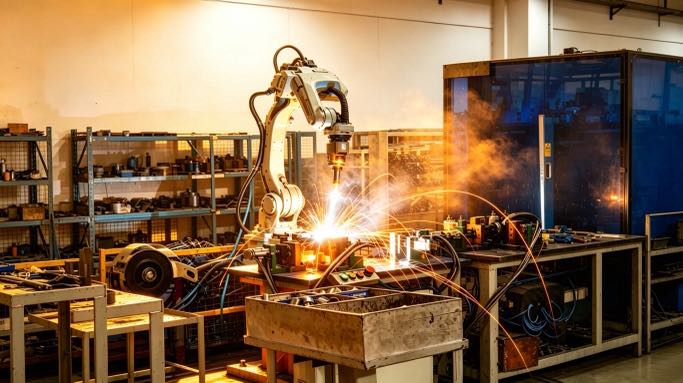
The welding process consists of four steps:
1. Laser Generation: Fiber lasers are the mainstream choice, operating at a wavelength of approximately 1070 nm and power ranging from 500 W to over 6 kilovatios. Raycus、MAX Photonics fiber lasers achieve an electro-optical conversion efficiency of over 40%, with the ECO series exceeding 35%, far surpassing traditional CO₂ lasers (aproximadamente 10%). They are energy-efficient and stable.
2. Beam Transmission: The laser is transmitted through a 50-200 μm fiber optic cable to the robotic welding head, with virtually no energy loss and no impact from joint movement.
3. Focusing and Positioning: The welding head focuses the beam into a 0.2–0.8 mm spot with an energy density as high as 10⁶–10⁷ W/cm², capable of melting metal in milliseconds. 6-axis robots achieve repeatability of ±0.05 mm (Fanuc, LLORAR, TEJIDO, etc.).
4. Melt Pool Formation and Solidification: The laser creates a “keyhole” effect, generating a vapor channel within the metal surrounded by a liquid melt pool. Heating and cooling rates are extremely fast (10³–10⁶ °C/s), with a heat-affected zone of only 0.1–1 mm.
Technical Highlights: Supports self-fusion welding without the need for filler wire, eliminating the risk of material composition inconsistencies.
Core Components and Configuration Options
Industrial-grade systems consist of five core modules:
| Componente | Función | Typical Specifications | Selection Criteria |
| Laser | Generates laser energy | Fiber laser, 1–6 kW+ | Select power based on material thickness and speed |
| Industrial Robot | Executes motion paths | 6-eje, payload 10–50 kg | Covers the total weight of the welding head and cables |
| Cabezal de soldadura láser | Focuses the beam | Collimating lens 100/150 milímetros, focusing lens 150–300 mm | Long focal length suitable for deep cavities; short focal length suitable for high speeds |
| Sistema de control | Coordinates movements | SOCIEDAD ANÓNIMA + Dedicated software | Supports real-time power modulation |
| Safety Protection(Optional) | Laser protection | Class 4 recinto de seguridad + Interlocks | Complies with IEC 60825-1 standard |
Optional high-end configurations: Vision-based weld seam tracking (±0,1mm), OCT online penetration depth monitoring, and oscillating welding head (to reduce gap sensitivity).
Key Application Scenarios and Case Studies
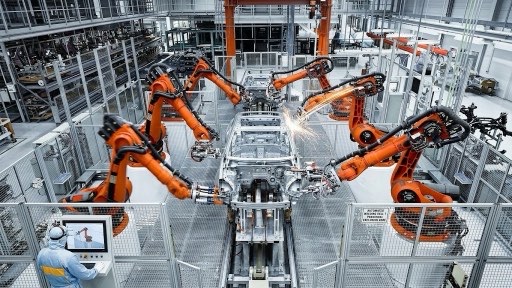
1. Automotive Manufacturing: White body side panels, doors, B-pillars, etc.. Materials include galvanized steel, acero al boro conformado en caliente, and 6000-series aluminum. A European luxury automaker has deployed multiple systems on its electric vehicle platform, achieving a welding speed of 90 mm/s and an annual production capacity exceeding 100,000 unidades.
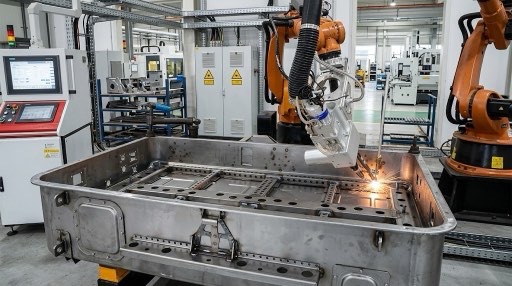
2. Power Batteries: Busbars, tabs, and pressure relief valves. Materials include red copper, aluminio, and copper-aluminum dissimilar metals. A leading battery manufacturer has deployed over 200 sistemas, with a single-line capacity of 200 ppm and a defect rate below 0.3%.
3. Dispositivos médicos: Pacemaker housings, surgical instruments. Materials include Ti6Al4V and 316L stainless steel. Welds are contamination-free, rework rates have dropped from 4.2% a 0.6%, and the process is ISO 13485 certified.
4. Consumer Electronics: Smartphone mid-frames, headphone contacts. Weld width: 0.3 milímetros; aesthetically pleasing with a small heat-affected zone, allowing for anodizing without grinding.
Clarification of Common Misconceptions
Q1: Is robotic laser welding limited to thin sheets?
Q2: Does robotic laser welding have to be performed in a dust-free environment (cleanroom)?
Q3: Robotic laser welding equipment is extremely expensive—can small factories afford it?
Q4: Is robotic laser welding very complex to operate, requiring professional welding engineers?
Q5: Does laser welding require any shielding gas?
Preguntas frecuentes
Q1: How fast is the welding speed? Typical data: 1 mm stainless steel at 80–120 mm/s (1 kilovatios); 2 aleación de aluminio mm: 40–60 mm/s (2 kilovatios); 0.3 mm copper foil: 150–200 mm/s (pulsed mode). Actual speeds require optimization based on material and power.
Q2: What is the approximate initial investment? An entry-level complete system (1 kW laser + small 6-axis robot + welding head + recinto de seguridad) costs approximately $30,000–$80,000.
Q3: Is it difficult to learn? Operator training typically takes 1–2 weeks and covers offline programming, laser safety, and parameter adjustment. Basic knowledge of metals is sufficient; no background as a professional welding engineer is required.
Q4: Is the weld strength lower than that of MIG welding? The strength of self-fusion laser welds typically reaches 90%–100% of the base material. When there is a gap, strength can be enhanced through oscillating welding or wire-fed laser welding.
Q5: Which safety standards are met? These primarily include IEC 60825-1 (Safety of laser products) y ISO 11553 (Safety of laser processing machines). The equipment must be equipped with a Class 4 recinto de seguridad, interlock switches, and emergency stop devices.
Referencias
IPG Photonics Fiber Laser Welding Guide
TRUMPF Automotive Laser Welding
Global Market Insights Robotics Laser Welding Report
CEI 60825-1:2014
Disclaimer: The information in this article is for reference only; actual results require verification through sample testing.
Identificación del autor
Este artículo está basado en la Federación Internacional de Robótica. (IFR) Informe Mundial de Robótica 2025, Sociedad Americana de Soldadura (AWS) datos de la fuerza laboral, y hojas de ruta tecnológicas de los principales fabricantes.
Autor:
Un experto en integración de sistemas de soldadura robótica con más de 12 años de experiencia en la industria. mi empresa ha terminado 26 años de experiencia profesional, tiene más de 40 tecnologías patentadas, y ha completado con éxito más de 1,500 proyectos en todo el mundo (aproximadamente 70% de los cuales se trataba de células de soldadura robóticas, totalizando más de 1,000 unidades). La empresa cuenta con la certificación CE de la UE. (Certificado No.: M.2026.206.C134866) y cumple con la EN 60204-1:2018 y ENISO 12100:2010 estándares. He ayudado a numerosas empresas manufactureras durante todo el proceso de implementación de estaciones de trabajo de soldadura robótica., desde la selección hasta el lanzamiento de la producción.
Actualizado: Puede 2026
PUBLICACIONES RELACIONADAS

Cómo un posicionador de soldadura controla la gravedad: La física de la estabilidad del charco y la calidad de la soldadura

¿Por qué agregar un robot del séptimo eje?? 5 Formas poderosas de aumentar la productividad & Reducir costos en 2026

Estación de trabajo de soldadura llave en mano: Del dibujo a la celda lista para producción

Análisis del ROI de la soldadura láser robótica: ¿Vale la pena la inversión??

Posicionador de soldadura en venta: Cómo elegir el tipo adecuado para su pieza (Contrapunto, Tipo L, Tipo U, 3 ejes horizontales, Rotativo de un solo eje, Inclinación vertical)
