Custom Robot Workstations And Laser Systems Manufacturer



Real-World Robotic Welding Cell Applications in General Industry: Case Studies 2026
Beyond Automotive — Robotic Welding Cell in General Industry
While automotive manufacturing is the star application for robotic welding, robotic welding cells are also widely used in general industry.
According to the International Federation of Robotics (IFR) 2025 report, welding applications account for approximately 21% of global industrial robot installations — a significant portion deployed in non-automotive general industry: steel structure, construction machinery, agricultural equipment, metal furniture, pressure vessels, pipe, hardware, and more.
These industries share common challenges: smaller batch sizes than automotive, lower margins, yet the same pressures from welder shortages and inconsistent quality.
This article presents three real (anonymized) general-industry application cases, showing the actual performance and value of robotic welding cells across different scenarios.
Case 1: Steel Structure Fabrication Shop — Large Component Welding Efficiency Improvement
Company Background
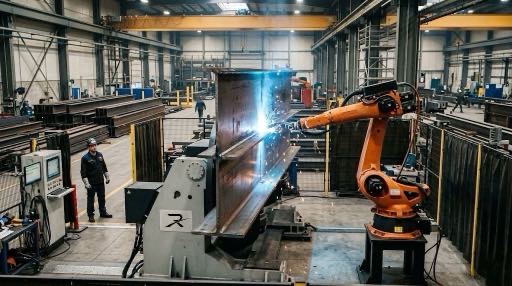
A mid-sized steel structure fabrication shop in East China, producing steel beams, columns, and trusses for construction. Annual output value: approximately $12 million USD.
Main pain points before deployment: Difficulty hiring welders. Large components required frequent flipping and repositioning. Multi-angle welding depended heavily on skilled welders. Weld quality was inconsistent with high rework rates.
Deployment
Introduced a two-station robotic welding cell in early 2025, configured with:
- 6-axis industrial robot (16kg payload, 1.8m reach)
- Dual-axis servo positioner (L-type, 2-ton capacity)
- Seam tracking system
- Safety fencing + light curtain interlock
- Total investment: approximately $150,000 USD
Before/After Data Comparison
| Metric | Before (Manual) | After (Robotic) | Change |
| Single weld seam time | 18 minutes | 6.8 minutes | ~2.65x productivity gain |
| First-pass weld acceptance rate | 91% | 98.50% | +7.5 percentage points |
| Welder requirement | 6-7 welders | 2 operators + 1 QC | ~57% reduction |
| Annual production capacity | Baseline | 62% | Significant increase |
| Payback period | — | 14 months | — |
Key Success Factors
The L-type dual-axis positioner combined with the seam tracking system effectively solved the challenge of multi-angle, multi-position welding on large steel structures. The robot automatically adapts to minor weld path deviations, ensuring consistent weld quality.
Case 2: Agricultural Machinery Manufacturer — High-Mix Low-Volume Flexible Production
Company Background
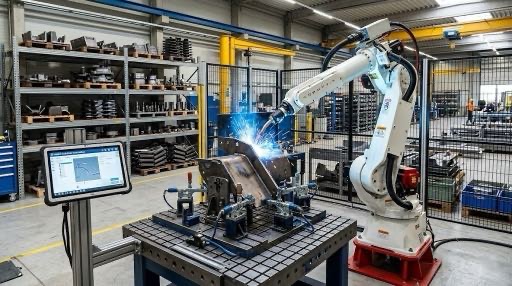
An agricultural machinery parts manufacturer in North China, producing rotary tiller blade holders, frames, and protective covers — over 200 different product specifications annually.
Main pain points before deployment: High product variety, small batch sizes, frequent changeovers. Each changeover took 1-2 hours for tooling and program adjustment. The welder workforce was aging, with few young replacements.
Deployment
Introduced a standard single-station robotic welding cell, configured with:
- 6-axis industrial robot (10kg payload)
- Quick-change tooling fixture system (modular design)
- Offline programming software
- Total investment: approximately $70,000 USD
Before/After Data Comparison
| Metric | Before (Manual) | After (Robotic) | Change |
| Changeover time | 45 minutes | 7-9 minutes | ~80% reduction |
| Daily output | Baseline | ~2.4x increase | — |
| Weld defect rate | Baseline | 65% reduction | — |
| Welding labor cost | Baseline | ~57% reduction | — |
| Payback period | — | 15 months | — |
Key Success Factors
The modular quick-change fixture system + offline programming dramatically improved flexibility for high-mix low-volume production. Operators can complete path planning on a computer and finish changeover within 15 minutes.
Case 3: Metal Furniture Manufacturer — Quality and Efficiency Improvement for Batch Frame Welding
Company Background
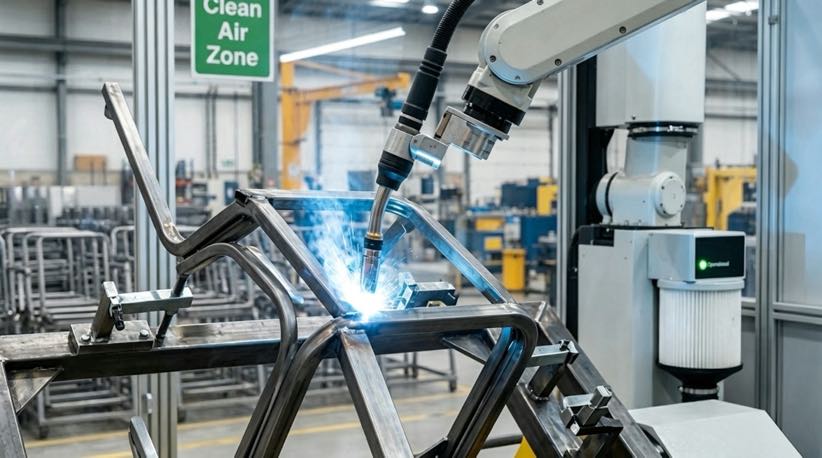
A metal furniture manufacturer in South China, producing office chair frames, shelving, and display stands — typical medium-batch production, primarily exporting to the European market. European customers had extremely high requirements for weld appearance consistency.
Main pain points before deployment: Welders’ skill levels varied significantly. The same chair model welded by different welders produced vastly different weld quality. Customer complaints about weld appearance. High return rates. High welding fume concentration, environmental pressure.
Deployment
Deployed a single-station robotic welding cell in 2025, configured with:
- 6-axis industrial robot (6kg payload)
- Pulse MIG welding power source
- Single-axis rotary positioner
- Standardized fixture system
- Torch-mounted fume extraction
- Total investment: approximately $60,000 USD
Before/After Data Comparison
| Metric | Before (Manual) | After (Robotic) | Change |
| Weld time per frame | 12 minutes | 4.5 minutes | ~2.7x productivity gain |
| Weld appearance consistency | Highly variable | Highly consistent | Dramatic improvement |
| Customer return rate | Baseline | 70% reduction | — |
| Welding production lines | 4 manual lines | 1 robotic cell + minor manual assist | — |
| Overall production capacity | Baseline | ~145% increase | — |
| Payback period | — | 12 months | — |
Key Success Factors
Standardized fixtures + stable pulse MIG welding parameters ensured the high weld appearance and consistency requirements for metal furniture, while significantly reducing worker physical strain. Torch-mounted fume extraction effectively improved the workshop environment.
Key Takeaways from All Three Cases
| Dimension | Case 1 (Steel Structure) | Case 2 (Ag Machinery) | Case 3 (Metal Furniture) |
| Primary pain point | Large components, multi-angle welding | Frequent changeovers, aging welders | Quality consistency, appearance requirements |
| Selection direction | Two-station + seam tracking | Single-station + quick-change tooling | Single-station + standardized fixtures |
| Typical investment | ~$150k USD | ~$70k USD | ~$60k USD |
| Payback period | 14 months | 15 months | 12 months |
| Biggest gain | 2.65x productivity gain | 80% faster changeover | 70% return rate reduction |
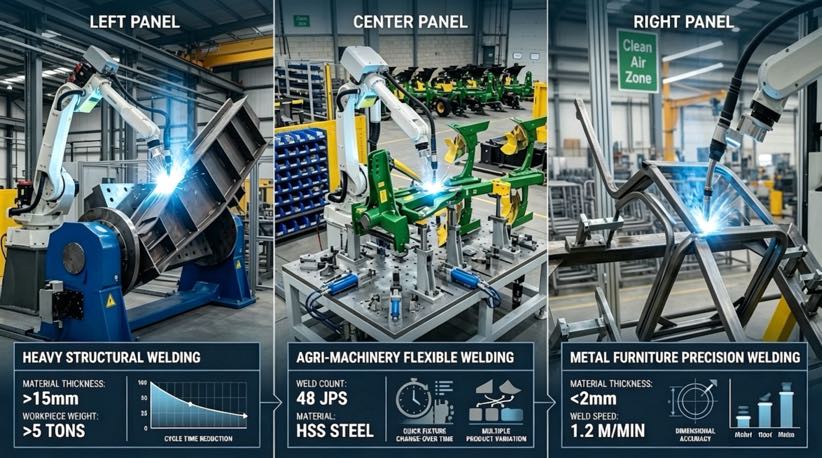
Common Success Factors for Robotic Welding Cell Deployment in General Industry
Match Selection to Production Characteristics
Large parts, low batch sizes → favor single-station. Stable batch sizes → favor two-station. Don’t overspecify — Case 2’s single-station solution fully met the high-mix low-volume needs with lower investment and faster payback.
Fixture Design Is Critical
Multiple cases prove that professional fixture investment often determines project success. The modular quick-change fixtures in Case 2 and standardized fixtures in Case 3 were key success factors. Budget 5-10% of total investment for fixture iterations.
Training and After-Sales Support
Operator training and responsive after-sales support are critical for long-term stable operation. All three companies received 1-2 weeks of on-site training, enabling operators to independently handle program recall, changeover, and basic troubleshooting.
Safety and Environmental Compliance
All deployments complied with ISO 10218-2 safety standards and included efficient fume extraction systems. Case 3 specifically used torch-mounted extraction, effectively improving workshop air quality.
These three real cases from steel structure fabrication, agricultural machinery, and metal furniture manufacturing fully demonstrate: robotic welding cells deliver exceptional practical value in general industry as well.
They not only significantly improve production efficiency and weld quality but also effectively address welder shortages and accelerate automation transformation.
For small-to-medium manufacturers planning to introduce automated welding, the key is selecting the right robotic welding cell configuration based on your product characteristics and production rhythm — not simply pursuing the most complex solution.
Next Steps
If you are considering introducing a robotic welding cell to your shop, please share the following information:
1. Your main product type (e.g., steel structure, machinery parts, metal furniture)
2. Typical part dimensions and daily output volume
3. Your biggest current pain point (labor shortage, quality instability, or low efficiency)
We will provide targeted initial recommendations based on our real-world experience.
Data Sources
– International Federation of Robotics (IFR) – World Robotics 2025 Report
– American Welding Society (AWS) – Welding Workforce Data
– Summary of experience from 1000+ robotic welding cell delivery projects
Related Reading
- How to Choose a Robotic Welding Cell? Single-Station vs. Two-Station
- 2026 Robotic Welding Cell Cost and ROI Analysis
- 10 Key Benefits of Implementing a Robotic Welding Cell in Your Shop
Author Identification
This article is based on the International Federation of Robotics (IFR) World Robotics Report 2025, American Welding Society (AWS) workforce data, and major manufacturer technology roadmaps.
Author:
An expert in robotic welding system integration with over 12 years of industry experience. My company has over 26 years of professional experience, holds more than 40 patented technologies, and has successfully completed over 1,500 projects worldwide (approximately 70% of which involved robotic welding cells, totaling more than 1,000 units). The company holds EU CE certification (Certificate No.: M.2026.206.C134866) and complies with the EN 60204-1:2018 and EN ISO 12100:2010 standards. I have assisted numerous manufacturing companies throughout the entire process of robotic welding workstation implementation, from selection to production launch.
Updated: May 2026
RELATED POSTS

Robotic Welding Cell Trends 2026–2030: AI, Machine Vision & The Future of Welding Automation
2026 Robot Positioner Buyer’s Guide: All 5 Types Compared — Head-and-Tailstock, L-Type, U-Type, and More
Robotic Welding Cell vs Traditional Welding Line: What Actually Changes on Your Shop Floor
Coordinated Motion Programming: Making Your Robot and Positioner Move as One Kinematic Chain

3D Vision Laser Seam Tracking Explained:From Point Cloud to Weld Path in Seconds