


Custom Robot Workstations And Laser Systems Manufacturer



Robot Positioner ROI: How Much Is Manual Welding Actually Costing You?
| ⚠️ Pricing Disclaimer Prices shown are from a documented installation and are provided for illustration purposes only. Final pricing is determined by project specification, payload requirements, robot brand compatibility, and current material costs — contact us for an up-to-date project quote. |
Most factory owners know what a Robot Positioner costs to buy. Very few know what manual welding is costing them to keep.
The repositioning time shows up nowhere on the income statement. The rework labor gets absorbed into overhead. The overtime hours are treated as a normal cost of doing business. The skilled welder who retired early because her back gave out is replaced with a recruitment fee and three months of reduced productivity — and that too disappears into the noise.
This article lays out the true cost picture of manual welding operations, the categories that most ROI conversations miss, and a real-world case study from an automotive Tier-2 installation — with every number independently verified.
| What this article covers: ① The five hidden costs of manual welding most shops undercount ② What a complete ROI picture actually includes — and what most models leave out ③ A worked example from an actual automotive Tier-2 installation — with every number verified ④ Three mistakes that make ROI calculations misleading |
Part 1: The 5 Hidden Costs of Manual Welding
Before any ROI conversation is meaningful, you need an honest baseline. These five cost categories are consistently undercounted in the shops we assess — and together, they typically represent 35–55% of total welding labor cost.
Hidden Cost #1: Repositioning Time
In manual large-workpiece welding, welders spend less than 35% of their working hours actually welding. The rest is repositioning — waiting for the crane, rigging the sling, rotating the component, clearing the load, and getting back to position. In shops welding components above 500 kg, each repositioning event takes 15–25 minutes.
| What this looks like in practice: Across a standard two-shift operation, welders can end up paying for thousands of non-arc hours per year, per station — hours spent waiting and repositioning rather than welding. At a typical loaded labor rate, this routinely adds up to a six-figure annual cost in repositioning overhead alone, before a single weld defect or overtime hour is counted. |
Hidden Cost #2: Rework and Scrap
Weld quality in manual operations varies with the welder’s fatigue level, the shift, and the welding position. Joints executed in overhead or vertical positions carry 2–4× the defect probability of flat-position welds. Industry data across fabrication shops shows manual rework rates of 5–15% on audited welds, with each rework event costing 3–5× the original weld labor.
On a typical shop’s annual weld labor spend, even a moderate rework rate translates into tens of thousands of dollars in direct rework cost — plus material scrap, NDT re-inspection, schedule disruption, and the downstream cost of delayed shipments.
Hidden Cost #3: Overtime
When repositioning consumes the majority of shift time and production targets are set against 100% of shift time, the gap has to be made up somewhere. In most shops, it is made up with overtime. Overtime at 1.5× the base rate on the hours that should have been productive is one of the most expensive symptoms of repositioning inefficiency — and one of the most normalized.
Hidden Cost #4: Occupational Injury and Turnover
Overhead and vertical welding, combined with repeated crane-assisted load handling, generates musculoskeletal injury at a rate significantly higher than most industrial trades. The financial impact comes in three forms: workers’ compensation claims, early retirement of experienced welders (whose knowledge cannot be easily replaced), and the recruitment and training cost of the replacement.
Industry occupational health data consistently places experienced welder replacement costs at $15,000–$35,000 per departure when recruitment fees, onboarding productivity loss, and training time are fully accounted for.
Hidden Cost #5: Lost Revenue from Capacity Constraints
When a welding station runs at 35% arc-on time instead of 80%, the shop produces fewer units per shift than it could. For shops with a full order book, that gap is not a ‘waste’ issue — it is a revenue constraint. Every component that cannot be shipped on time because the welding station is the bottleneck represents margin that was not captured. This is rarely quantified, but it is often the single largest number in the full cost picture.
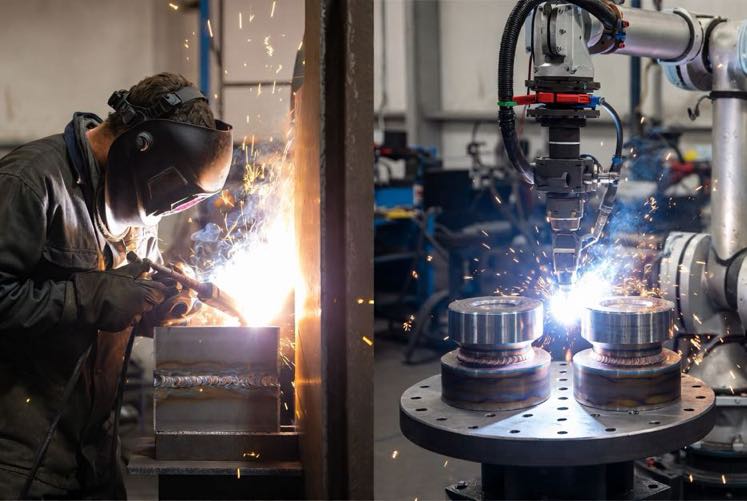
Part 2: What a Complete ROI Picture Actually Includes
Once the five hidden costs above are on the table, the ROI question changes shape. It’s no longer ‘what does the positioner cost’, but ‘what is the gap between what we’re paying now and what we’d pay after — and how fast does that gap cover the investment?’
A complete picture pulls together four cost categories that a Robot Positioner directly addresses:
- Repositioning labor — the non-arc time spent waiting, rigging, and rotating workpieces manually
- Rework and scrap — the cost of correcting welds that didn’t meet quality standards the first time
- Overtime premiums — the extra-cost hours used to make up for lost productive time
- Welder recruitment and turnover — the cost of replacing skilled welders lost to injury or burnout
Based on documented post-installation audits across our installation network, these categories see substantial — and consistent — reductions once a Robot Positioner is in place:
| Cost Category | Typical Reduction |
| Repositioning labor | ~85% |
| Rework & scrap | ~80% |
| Overtime premium | ~60% |
| Welder turnover | ~50% |
| ⚠️ On payback period: The investment side of this equation depends entirely on your project specification — configuration, payload, robot brand compatibility, and current material costs all factor in, and the correct figure includes far more than hardware list price (see Part 4). Rather than estimate this on generic numbers, our team can run the full calculation against your actual production data — see the custom analysis offer below. |
Part 3: Worked Example — Automotive Bracket Manufacturer
The following figures are drawn from pre- and post-installation records at a Tier-2 automotive supplier producing structural bracket assemblies. All financial figures have been independently verified. Investment figures reflect a specific historical project and are shown for illustration only.
| ⚠️ Pricing Disclaimer Figures shown are for illustration only. Pricing is project-specific — contact us for a quote based on your project specification, payload requirements, and robot brand compatibility. |
Pre-Installation Baseline
Before installation, this station was operating with a 29% arc-on time — well below the 35% baseline typical of manual large-workpiece welding — alongside an 11.4% defect rate and significant overtime to compensate for lost productive hours.
Post-Installation Results (6-Month Average, Annualized)
| Metric | Before | After | Change |
| Arc-on time | 29% | ✅ 84% | +55 percentage points |
| Overall defect rate | 11.4% | ✅ 1.8% | −84% |
| Monthly rework labor cost | $5,586 | ✅ $842 | −$4,744/month |
| Overtime hours per month | 48 hrs | ✅ 6 hrs | −88% |
| Throughput (units/month) | 28 units | ✅ 37 units | +32% |
Results Summary — Verified
Across the four core cost categories — repositioning, rework, overtime, and turnover — this installation produced a total identified annual saving of approximately $173,000, independently verified against arc-on audits, QC records, payroll data, and HR records.
Based on this client’s actual project investment, the simple payback period was 10.2 months on cost savings alone.
| Unquantified upside — throughput revenue: The 32% throughput increase was not included in the payback figure above. For this client, the additional production capacity translated to $185,000 in additional annual revenue, bringing true combined payback to approximately 6 months. Conservative recommendation: build your business case on the cost-saving payback alone, and present throughput revenue as additional validated upside. |
Part 4: 3 Mistakes That Make ROI Conversations Misleading
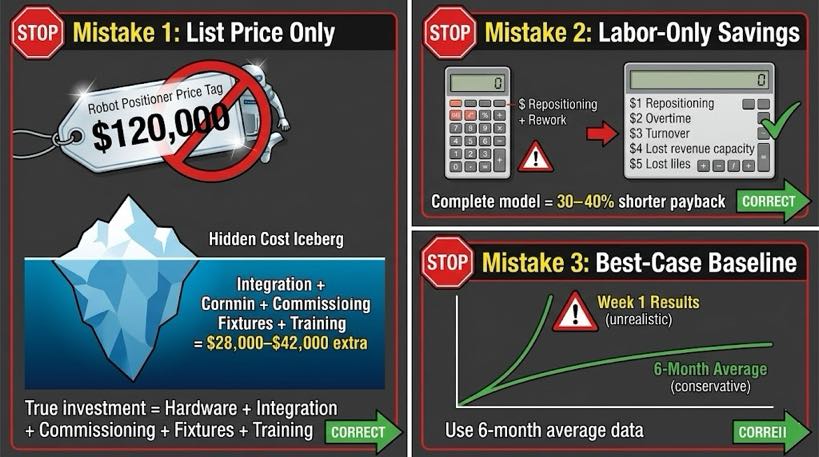
Mistake #1: Using Hardware List Price as the Investment Figure
The correct investment figure is: hardware + integration engineering + commissioning + fixture modification + training + spare parts + shipping and logistics.
In most projects, all non-hardware costs combined add 40–70% to the hardware price. A calculation based on list price alone produces an artificially optimistic payback period that the actual project will not match.
| Cost Component | Typical Range | Notes |
| Robot positioner hardware | Project-specific — request quote | Varies by configuration, payload, destination |
| Integration engineering | $15,000–$30,000 | Mechanical, electrical, software |
| Commissioning & testing | $8,000–$15,000 | On-site 2–4 days |
| Fixture modification | $5,000–$15,000 | Workpiece-dependent |
| Operator training | $2,000–$5,000 | Included with standard packages |
| Spare parts (Year 1) | $1,500–$3,000 | Servo drives, cables, encoder |
| Shipping & logistics | $2,000–$5,000 | DDP pricing available to US/EU/AU |
Mistake #2: Only Counting Direct Labor Savings
Most ROI conversations capture repositioning labor and rework labor. They miss overtime premiums, turnover costs, insurance impact from safety improvements, and — most significantly — the revenue value of additional production capacity.
A complete four-category model typically produces a payback period 20–30% shorter than a labor-only model. A model that also includes throughput revenue can show payback 40–50% shorter than the labor-only baseline.
Mistake #3: Using Best-Case Post-Installation Numbers
Arc-on time improvement takes 4–8 weeks to stabilize after commissioning. Defect rate reduction takes 1–3 months as programs are tuned. A credible business case should be built on 6-month average post-installation data, not first-week results.
Rule of thumb: if the conservative case — with savings 20% lower than projected — still pays back in under 18 months, the investment is defensible to any stakeholder.
Want Us to Run the Numbers on Your Operation?
If you’d like to understand exactly what a Robot Positioner could mean for your specific operation, our engineering team will build a custom analysis using your real production data:
- Provide your current production volume, shift structure, labor rate, and rework rate
- We assess which cost categories — repositioning, rework, overtime, turnover — represent your biggest opportunity
- We identify which Robot Positioner configuration produces the best results for your specific workpiece
- Written report delivered within 24 business hours, at no cost
| Request a Custom ROI Analysis for Your Welding Operation No obligation. 24-hour response. Delivered as a written analysis based on your actual numbers. |
Frequently Asked Questions
How do I calculate robot positioner ROI?
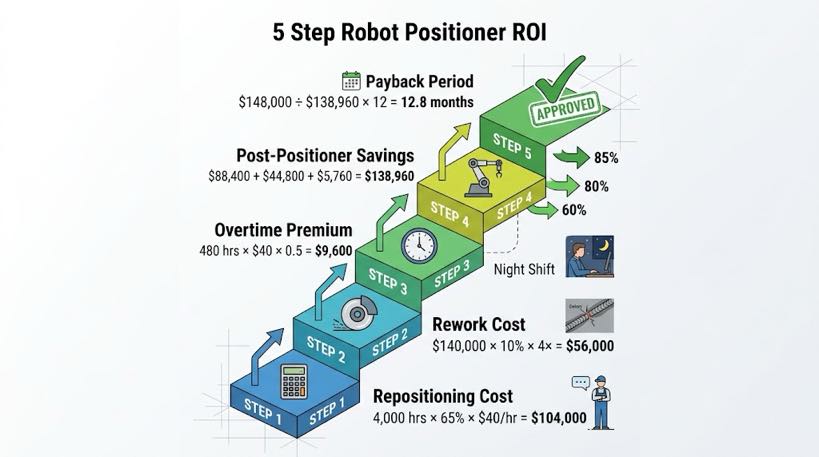
Start by quantifying your current annual costs across four categories: repositioning labor, rework and scrap, overtime premiums, and welder recruitment/turnover cost. Then compare these against documented post-installation reduction benchmarks — typically 85% for repositioning, 80% for rework, 60% for overtime, and 50% for turnover — to estimate your potential annual saving. From there, divide your total project cost (not just hardware price) by the annual saving and multiply by 12 to get payback in months. For an accurate result based on your own numbers, our team can run this analysis for you at no cost.
What is a realistic robot positioner payback period?
Based on verified post-installation audits across 200+ deployments, most robot positioner installations achieve full payback in 6–18 months under normal production conditions. The automotive bracket case study documented in this article achieved payback in 10.2 months on cost savings alone, and approximately 6 months when throughput revenue was included.
How much does a robot positioner project cost?
Project cost varies by product configuration, payload requirements, robot brand compatibility, and current material costs. The hardware price alone does not represent the full investment — integration, commissioning, fixtures, training, spares, and logistics typically add 40–70% on top. Contact us for a project-specific quote: we provide a full line-item cost breakdown within 24 business hours.
What reduction percentages should I use for savings estimates?
The conservative benchmarks from our installation network are: repositioning labor 85%, rework and scrap 80%, overtime premium 60%, and welder turnover 50%. These are 6-month average post-installation figures. For workpieces with simple geometry, results may be higher.
About the Author
Experience & Credentials
Robotic welding system integration specialist with 12+ years of direct project experience focused on Robot Positioner selection and integration. Has provided consulting to 300+ factories across North America, Europe, and Asia. All specification data in this article is drawn from actual H / B / L / U series product datasheets.
Company background: 26+ years of welding automation engineering, 40+ active patents, 1,500+ completed projects globally, approximately 70% involving Robot Positioner integration.
Certifications
- ISO 9001: 2015 (GB/T 19001-2016) — Quality Management System
- GJB 9001C-2017 — Military/Weapon Equipment Quality Management System
- EU CE — Machinery Directive 2006/42/EC (Cert. No. M.2026.206.C134866)
- High-Tech Enterprise — Cert. No. GR202341000595 (Issued Nov. 2023)
Last updated: Jun 2026
RELATED POSTS

7th Axis Robot vs Traditional Gantry: Which Is Better for Your Welding or Material Handling Line?

Robotic Laser Welding ROI Analysis: Is It Worth the Investment?

5 Reasons Large Workpiece Welding Is Inefficient — and How a Robot Positioner Solves Each One

Fixture-Free Fabrication: When a Welding Positioner Replaces Complex Jigs, Tack Welds, and Crane Time

Welding Positioner Types Compared: Headstock, L-Type, U-Type, 3-Axis & More
